EN
Certifications You Can Trust
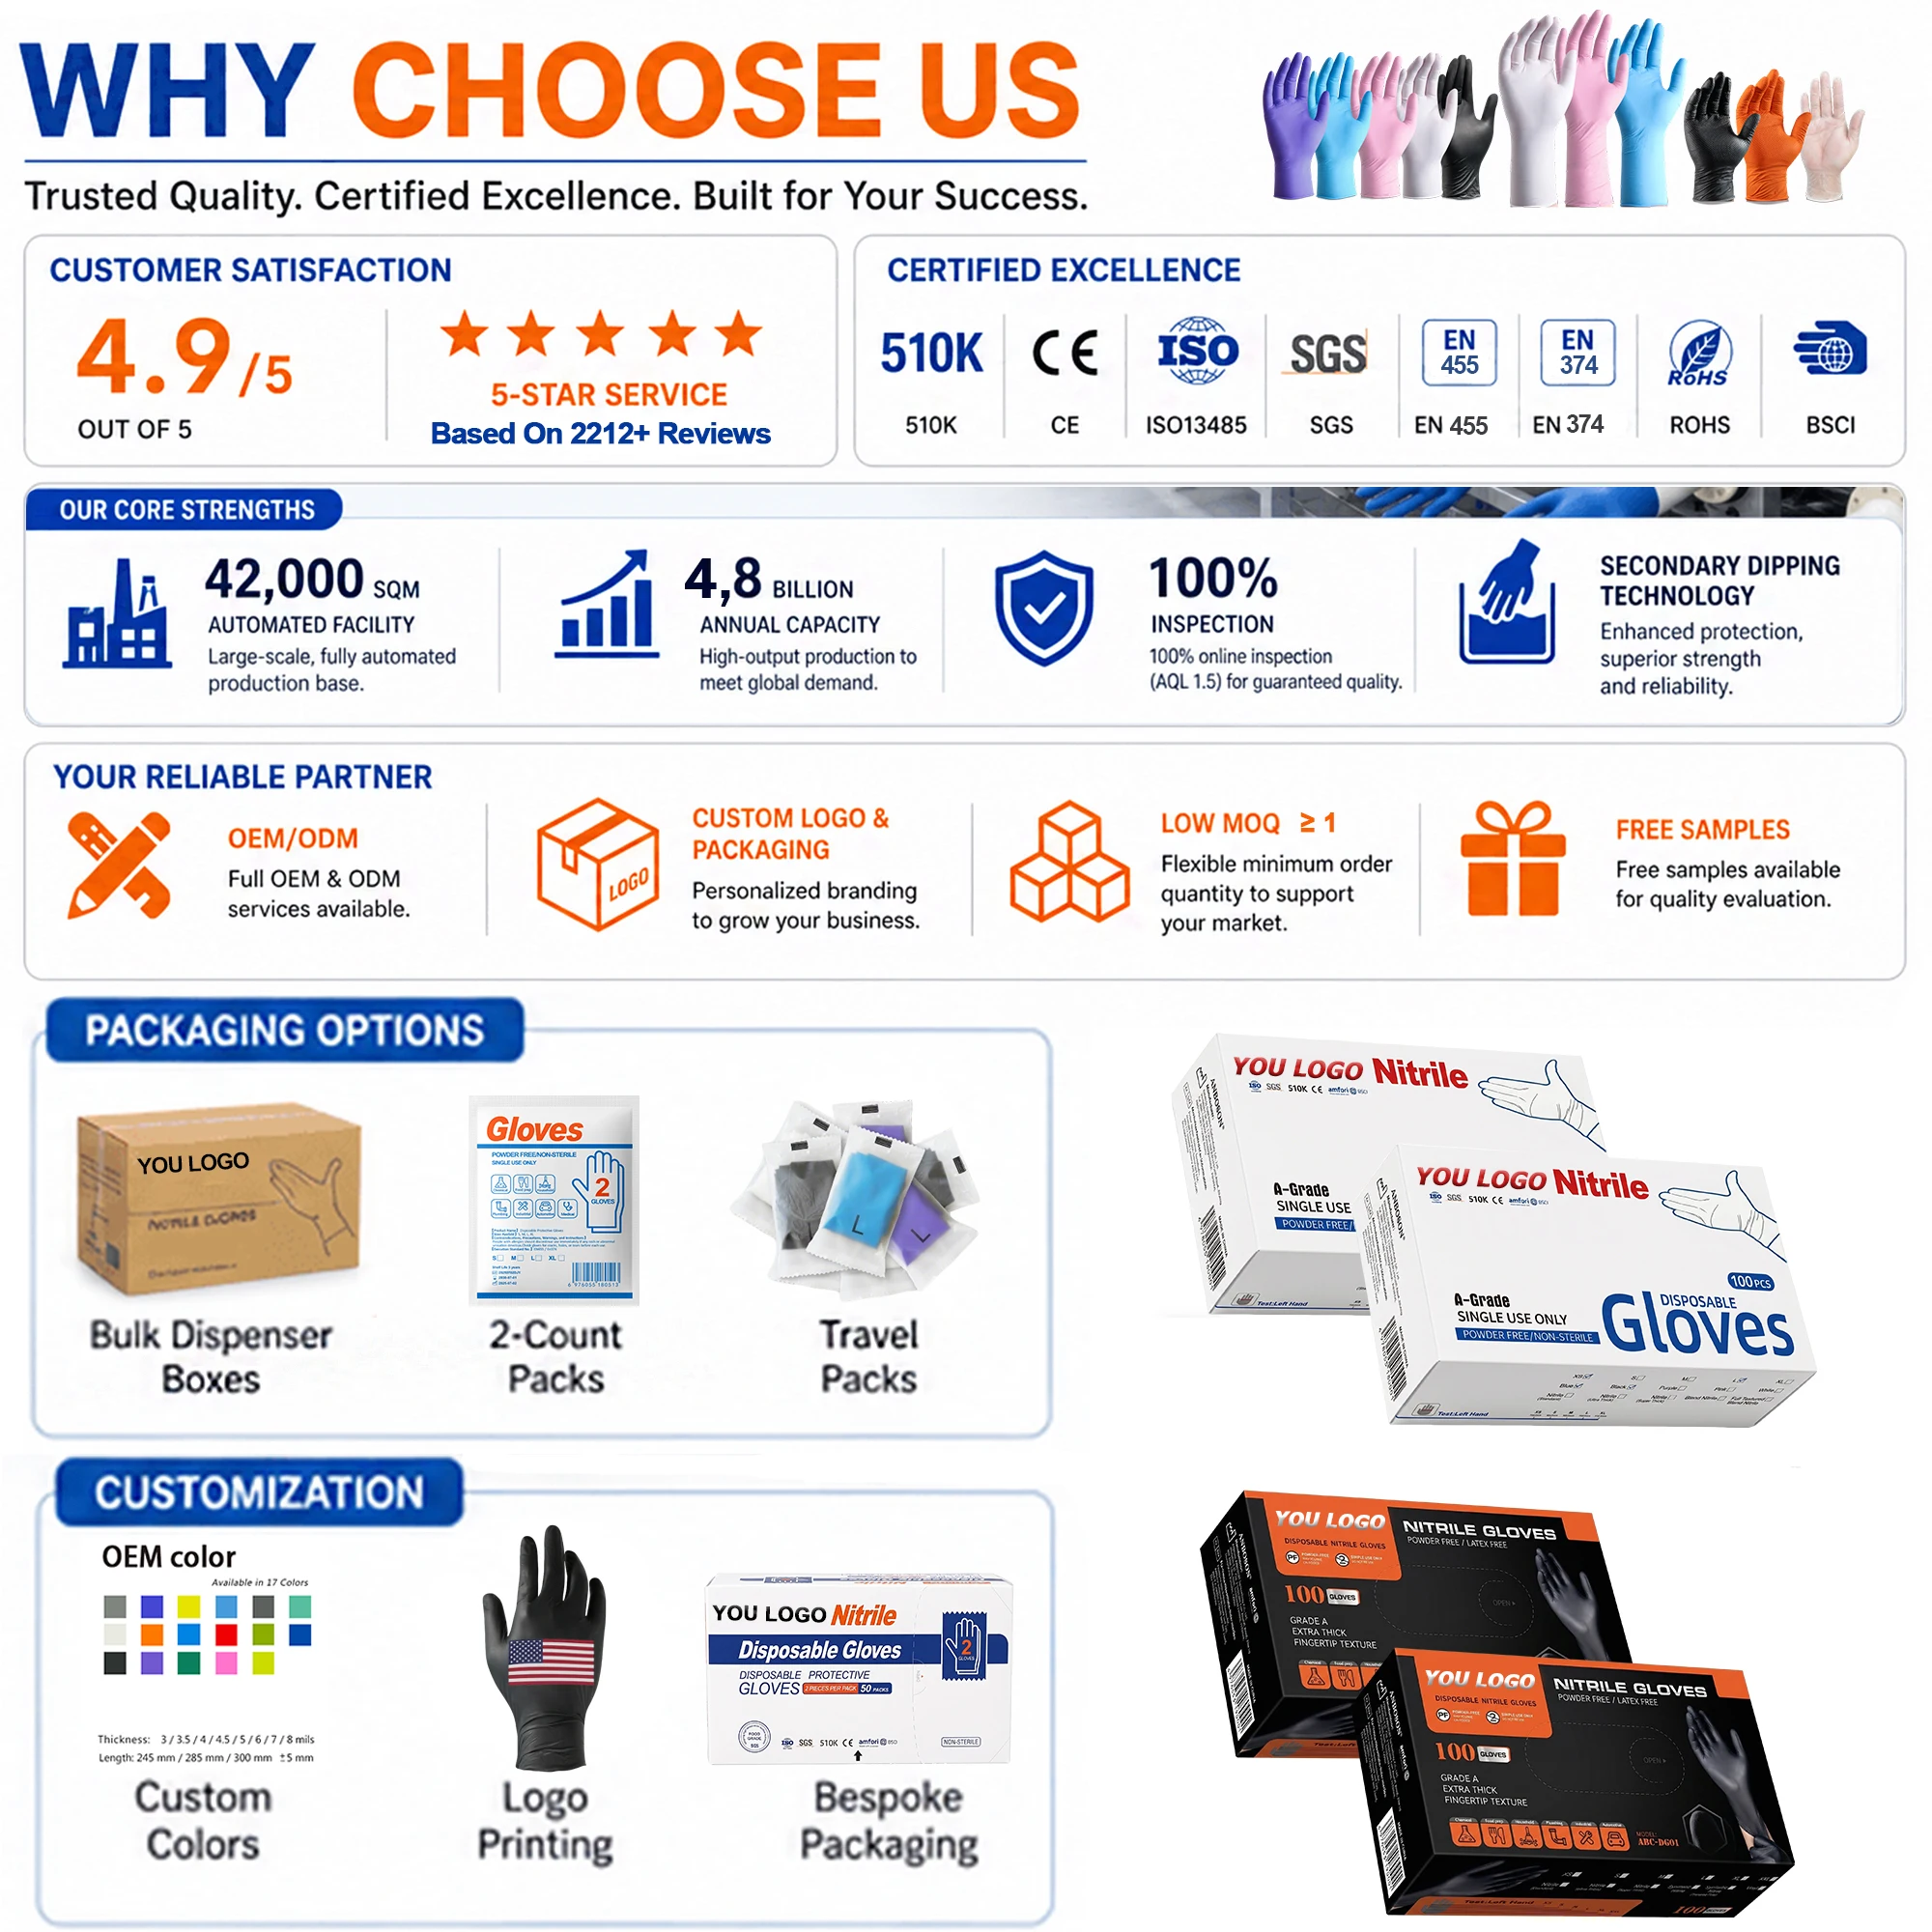
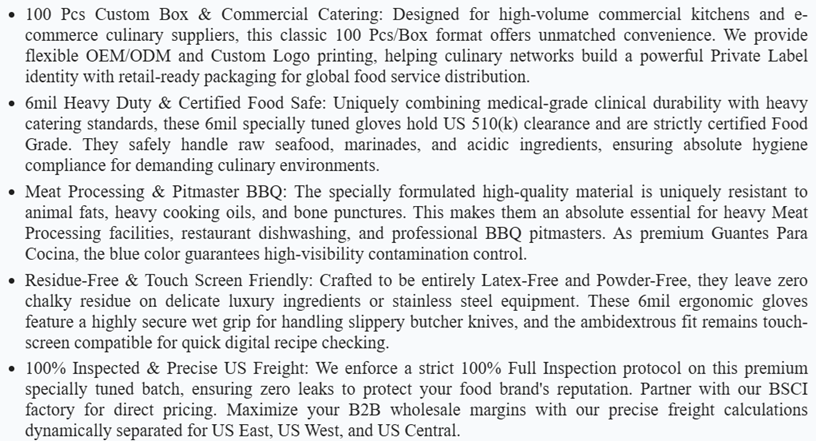
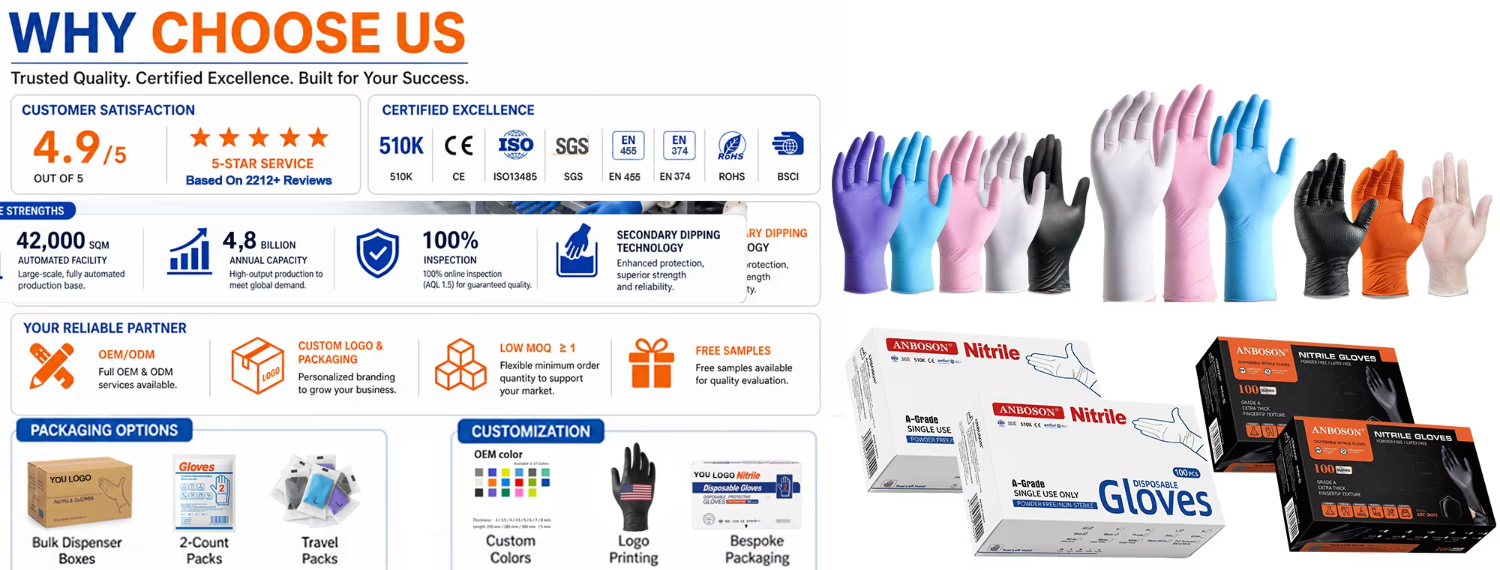
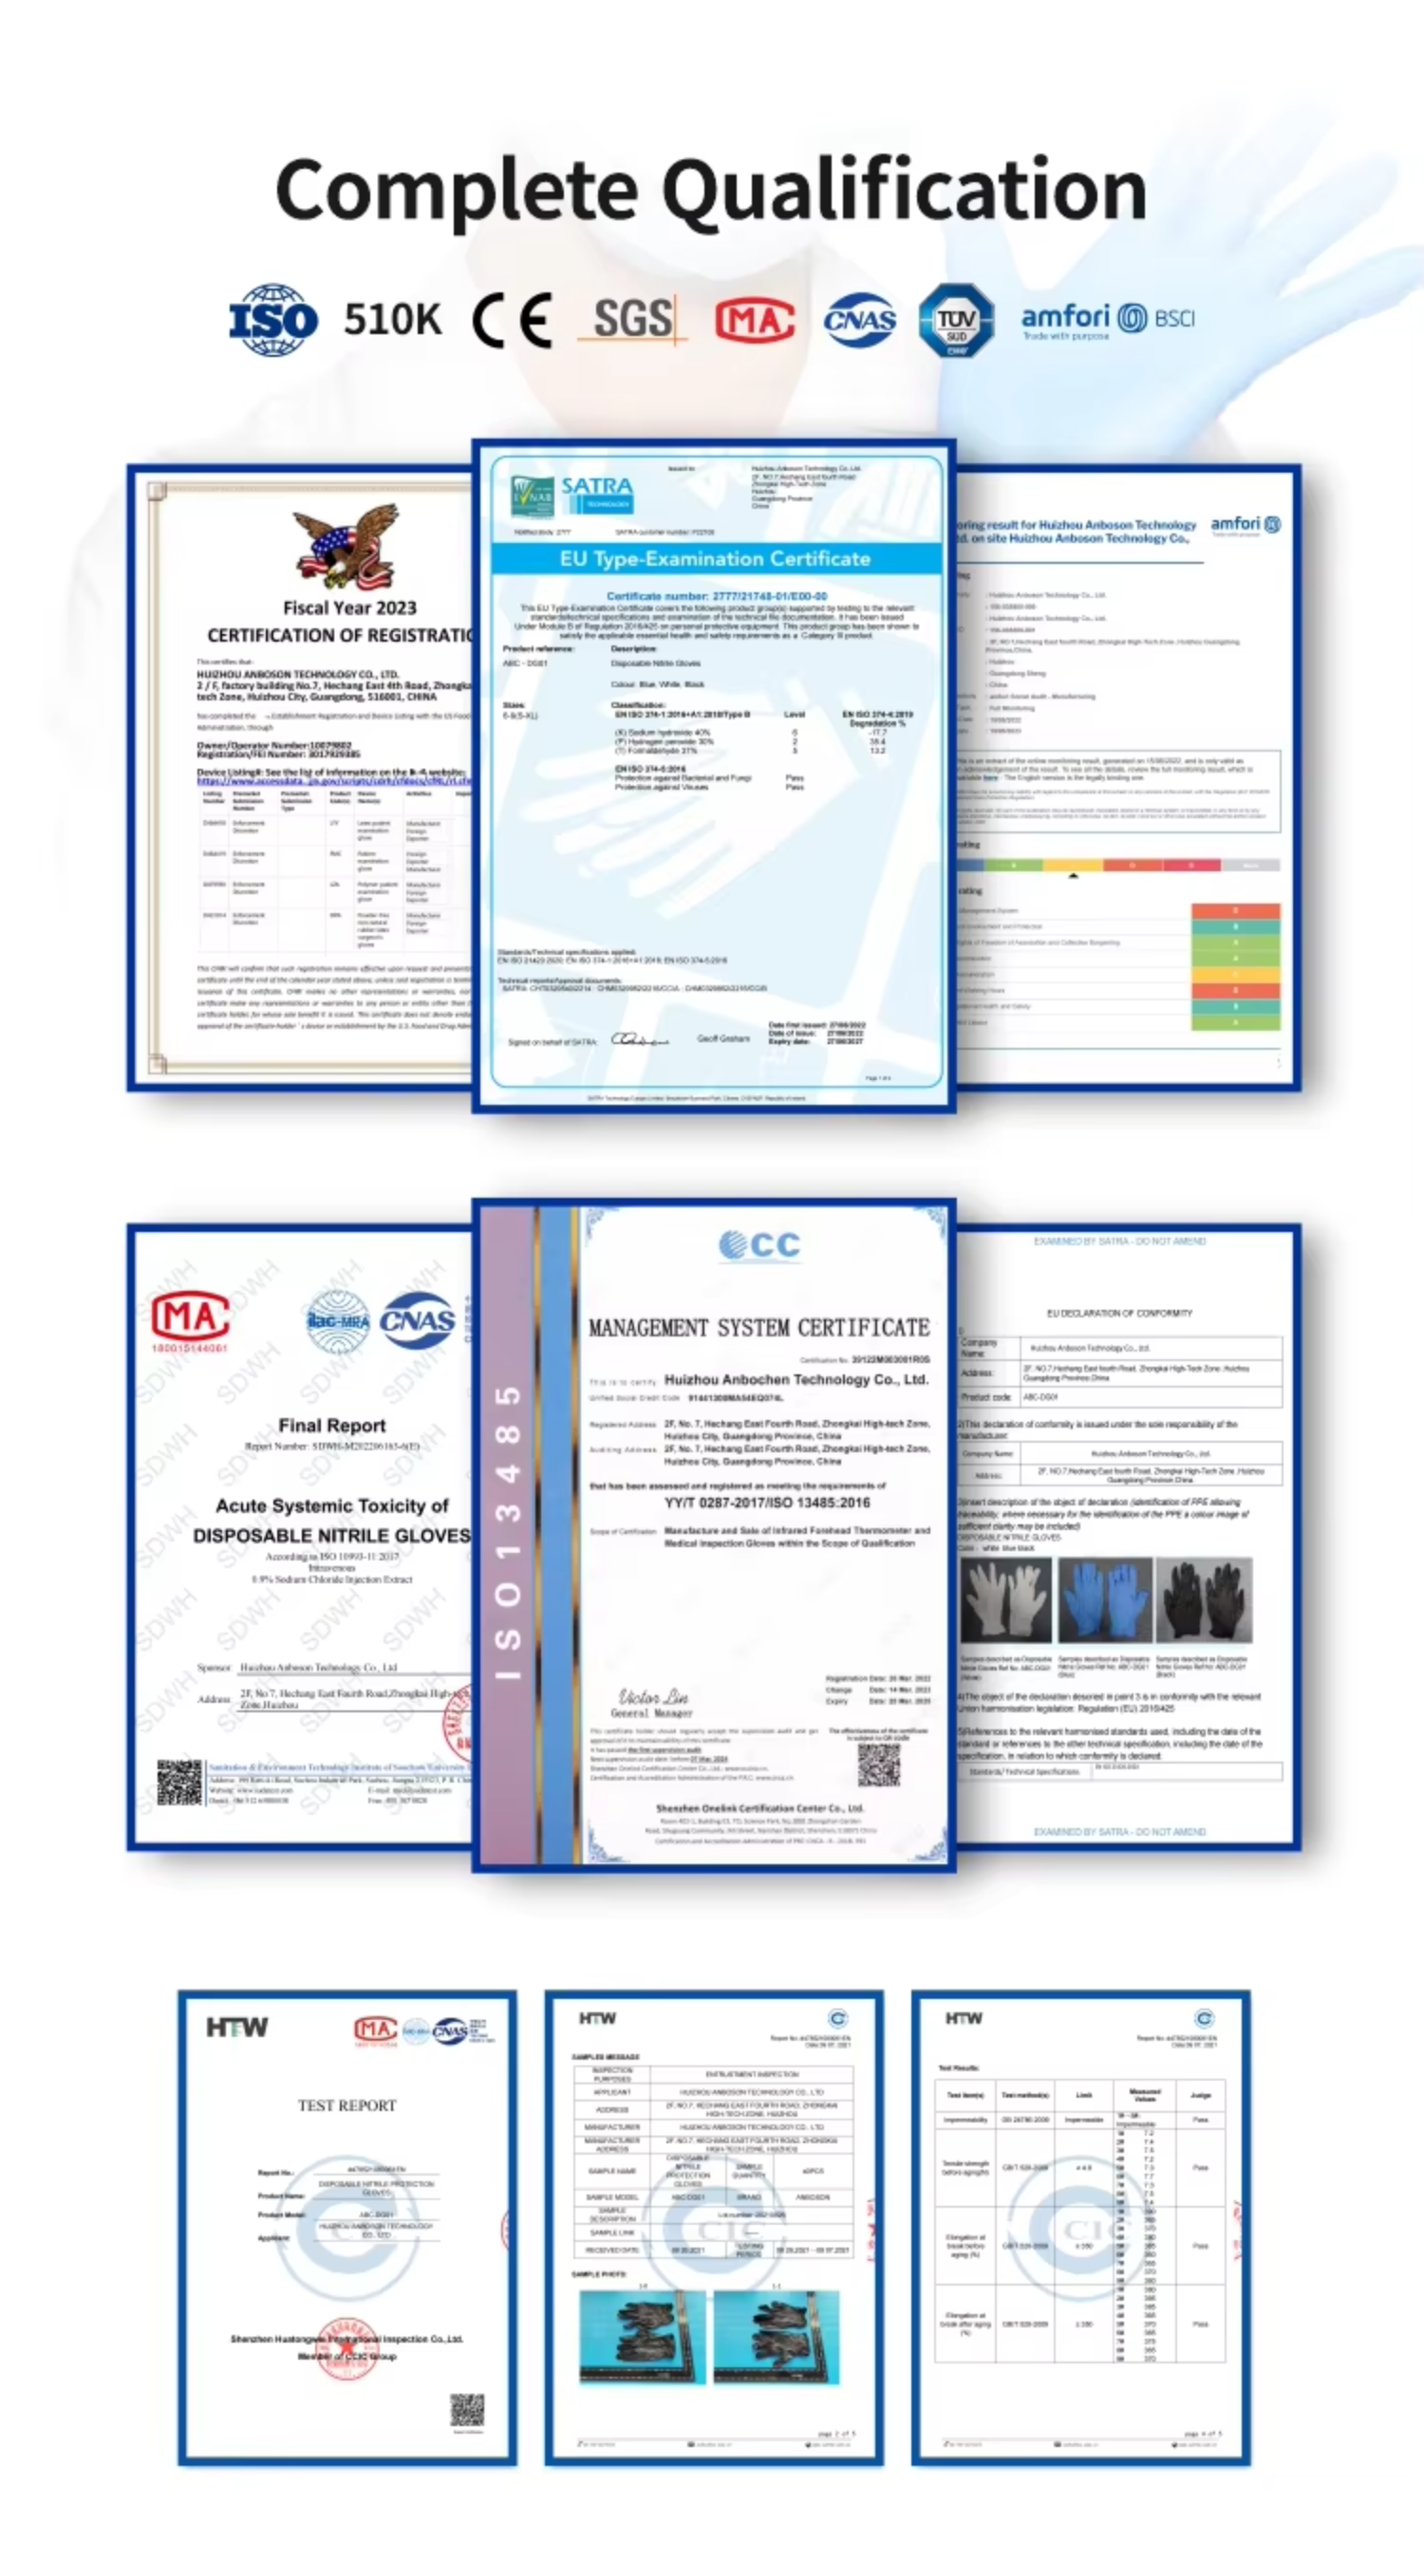
FDA 510K · CE · ISO 13485 · SGS — fully certified to meet global medical and industrial standards.


Are you manufacturer or trading company
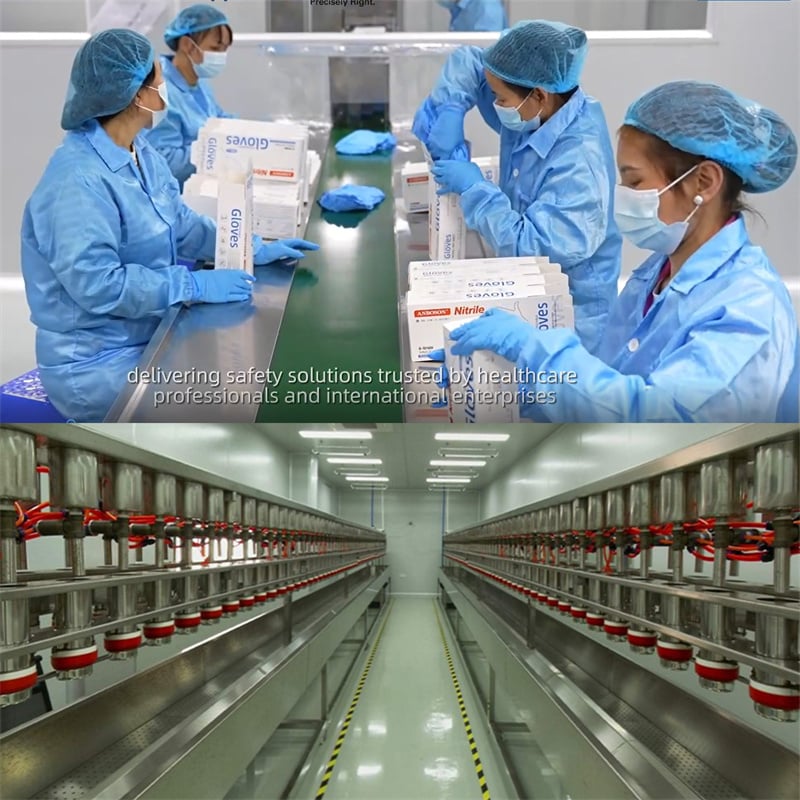
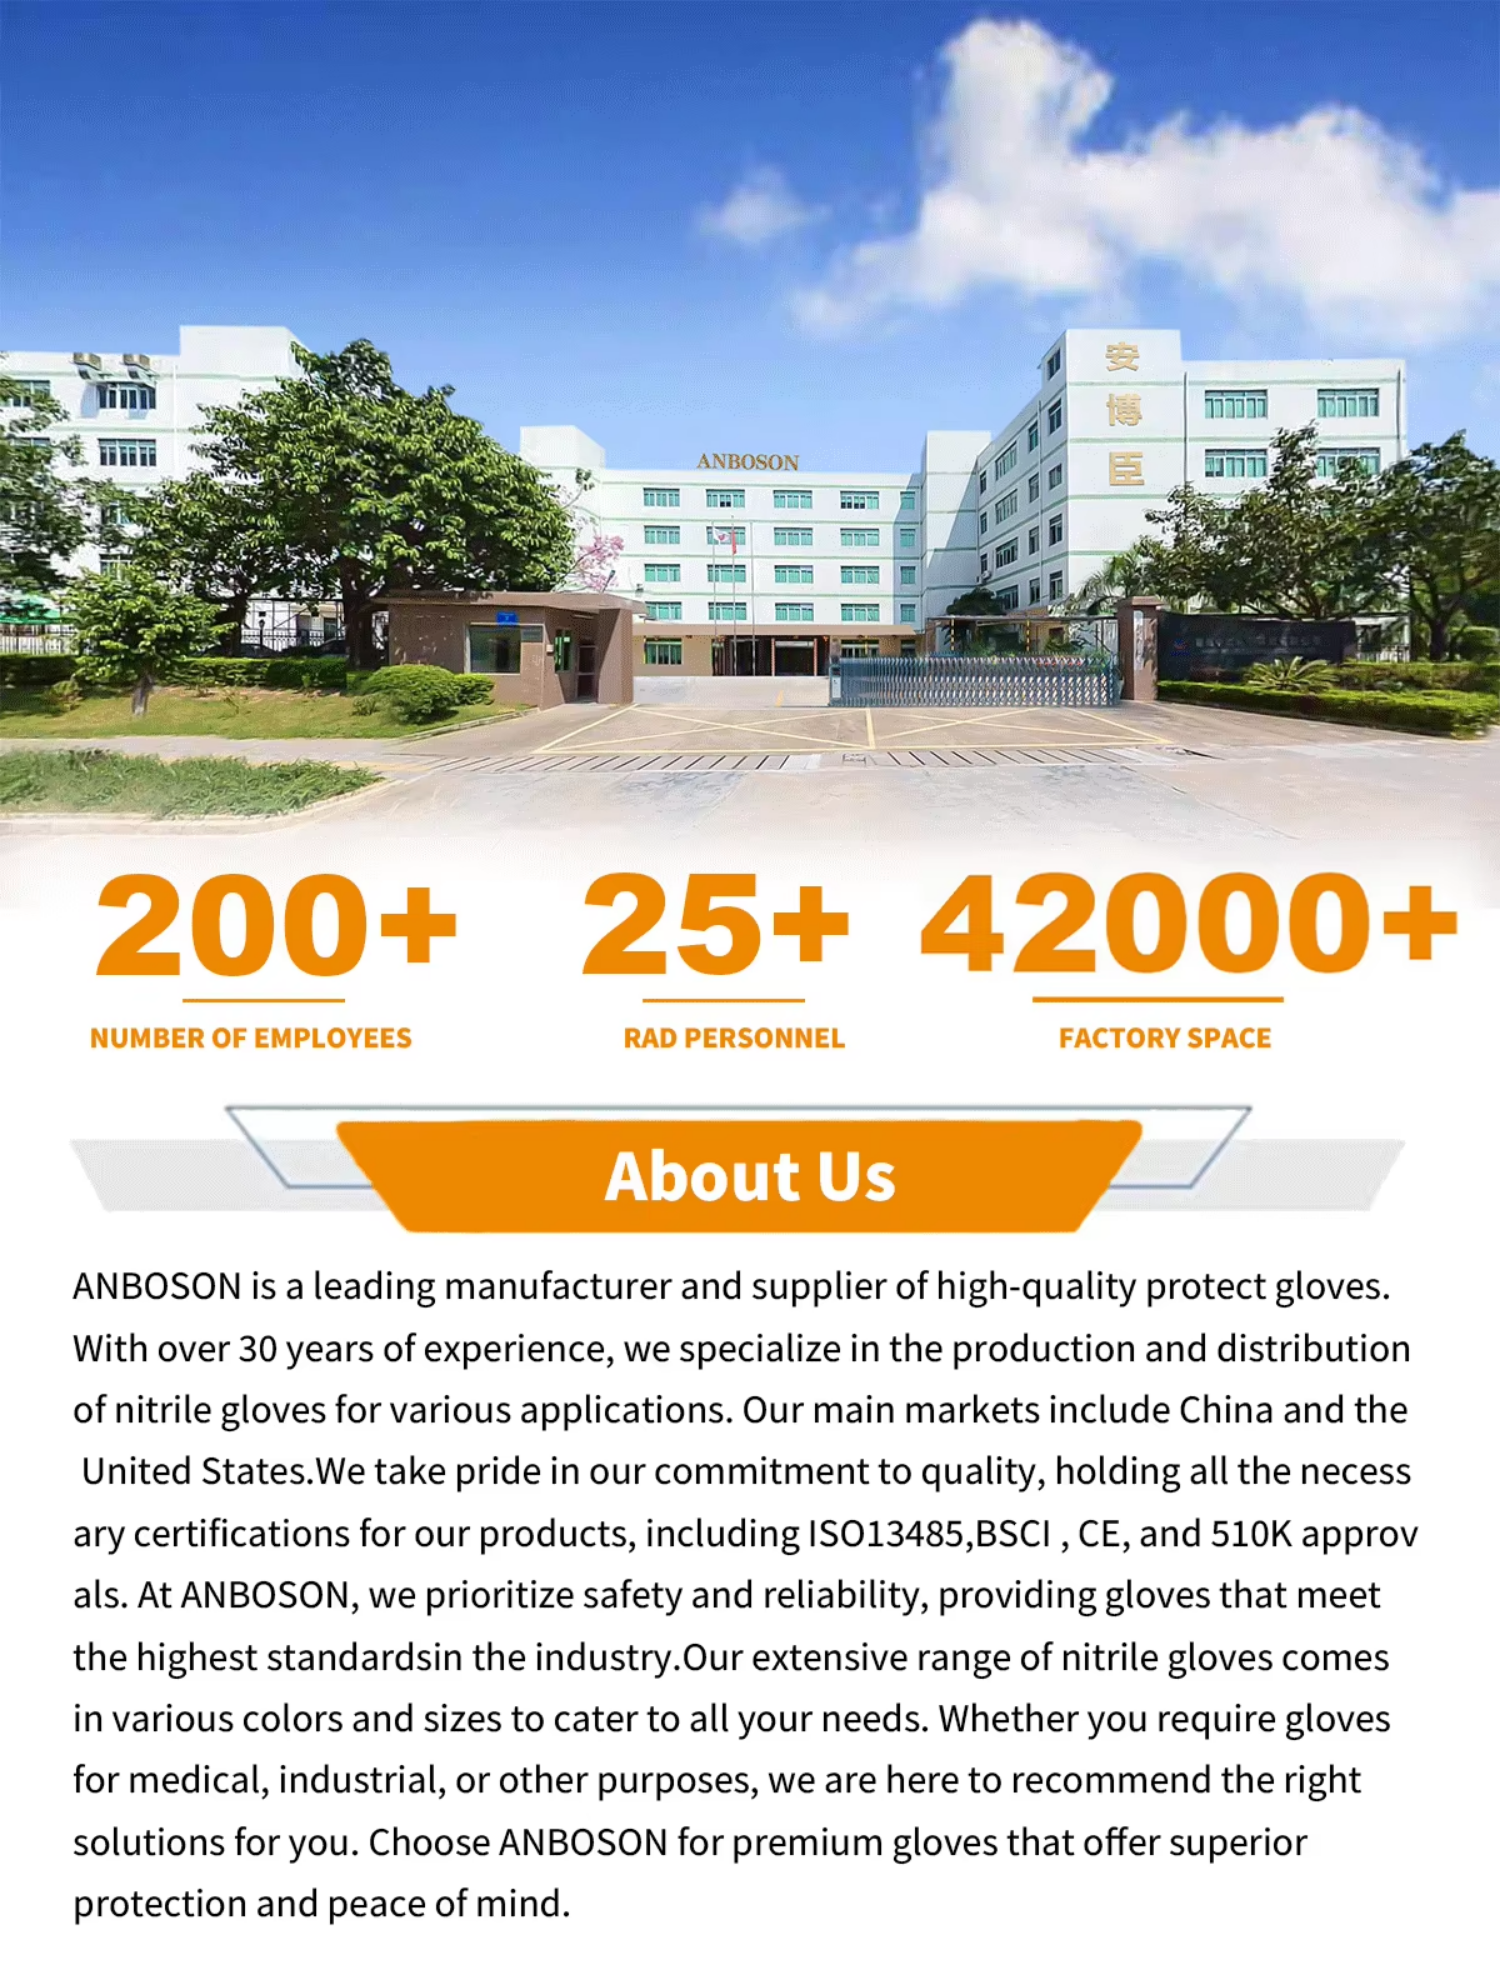
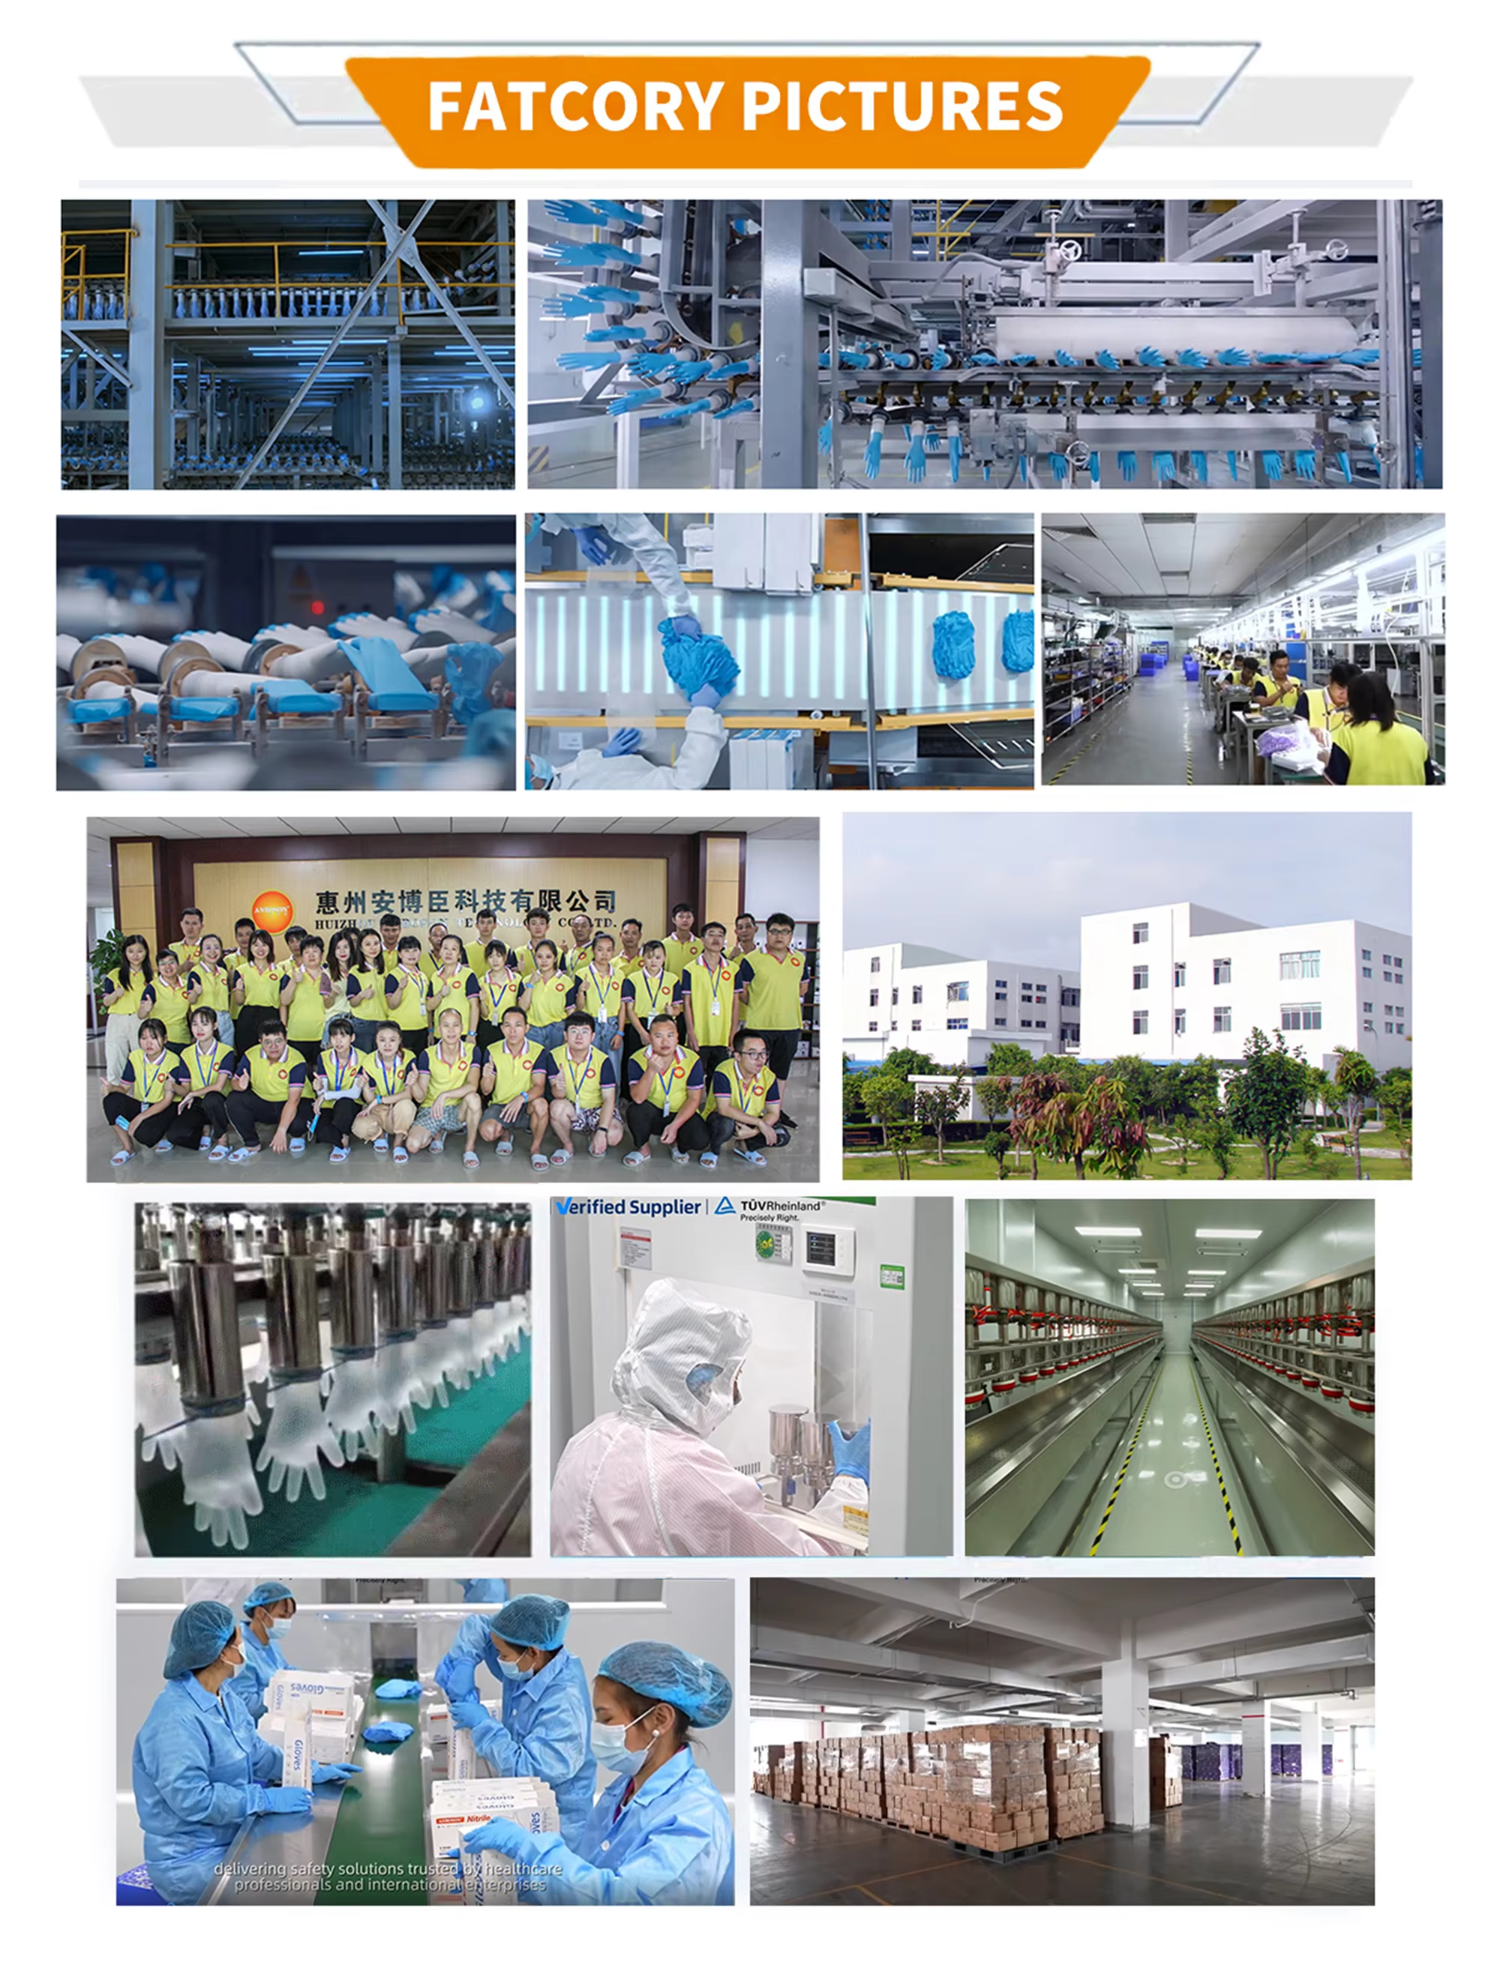
We are a professional manufacturer in Huizhou city Guangdong Province, China
What is your terms of payment
T/T 30% as deposit and 70% before delivery, & L/C at sight
What is your terms of delivery
EXW, FOB, CFR, CIF, DAP, DDP
How about your delivery time
Generally, our products are in stock and are ready to ship. Customized product order will take 10 to 25 days after receiving your advance payment. The specific delivery time depends on the items and the quantity of your order
How durable are these gloves? Will they rip easily
Depends on what you are doing while wearing them. They fit well, stay on your hands and they haven't ripped
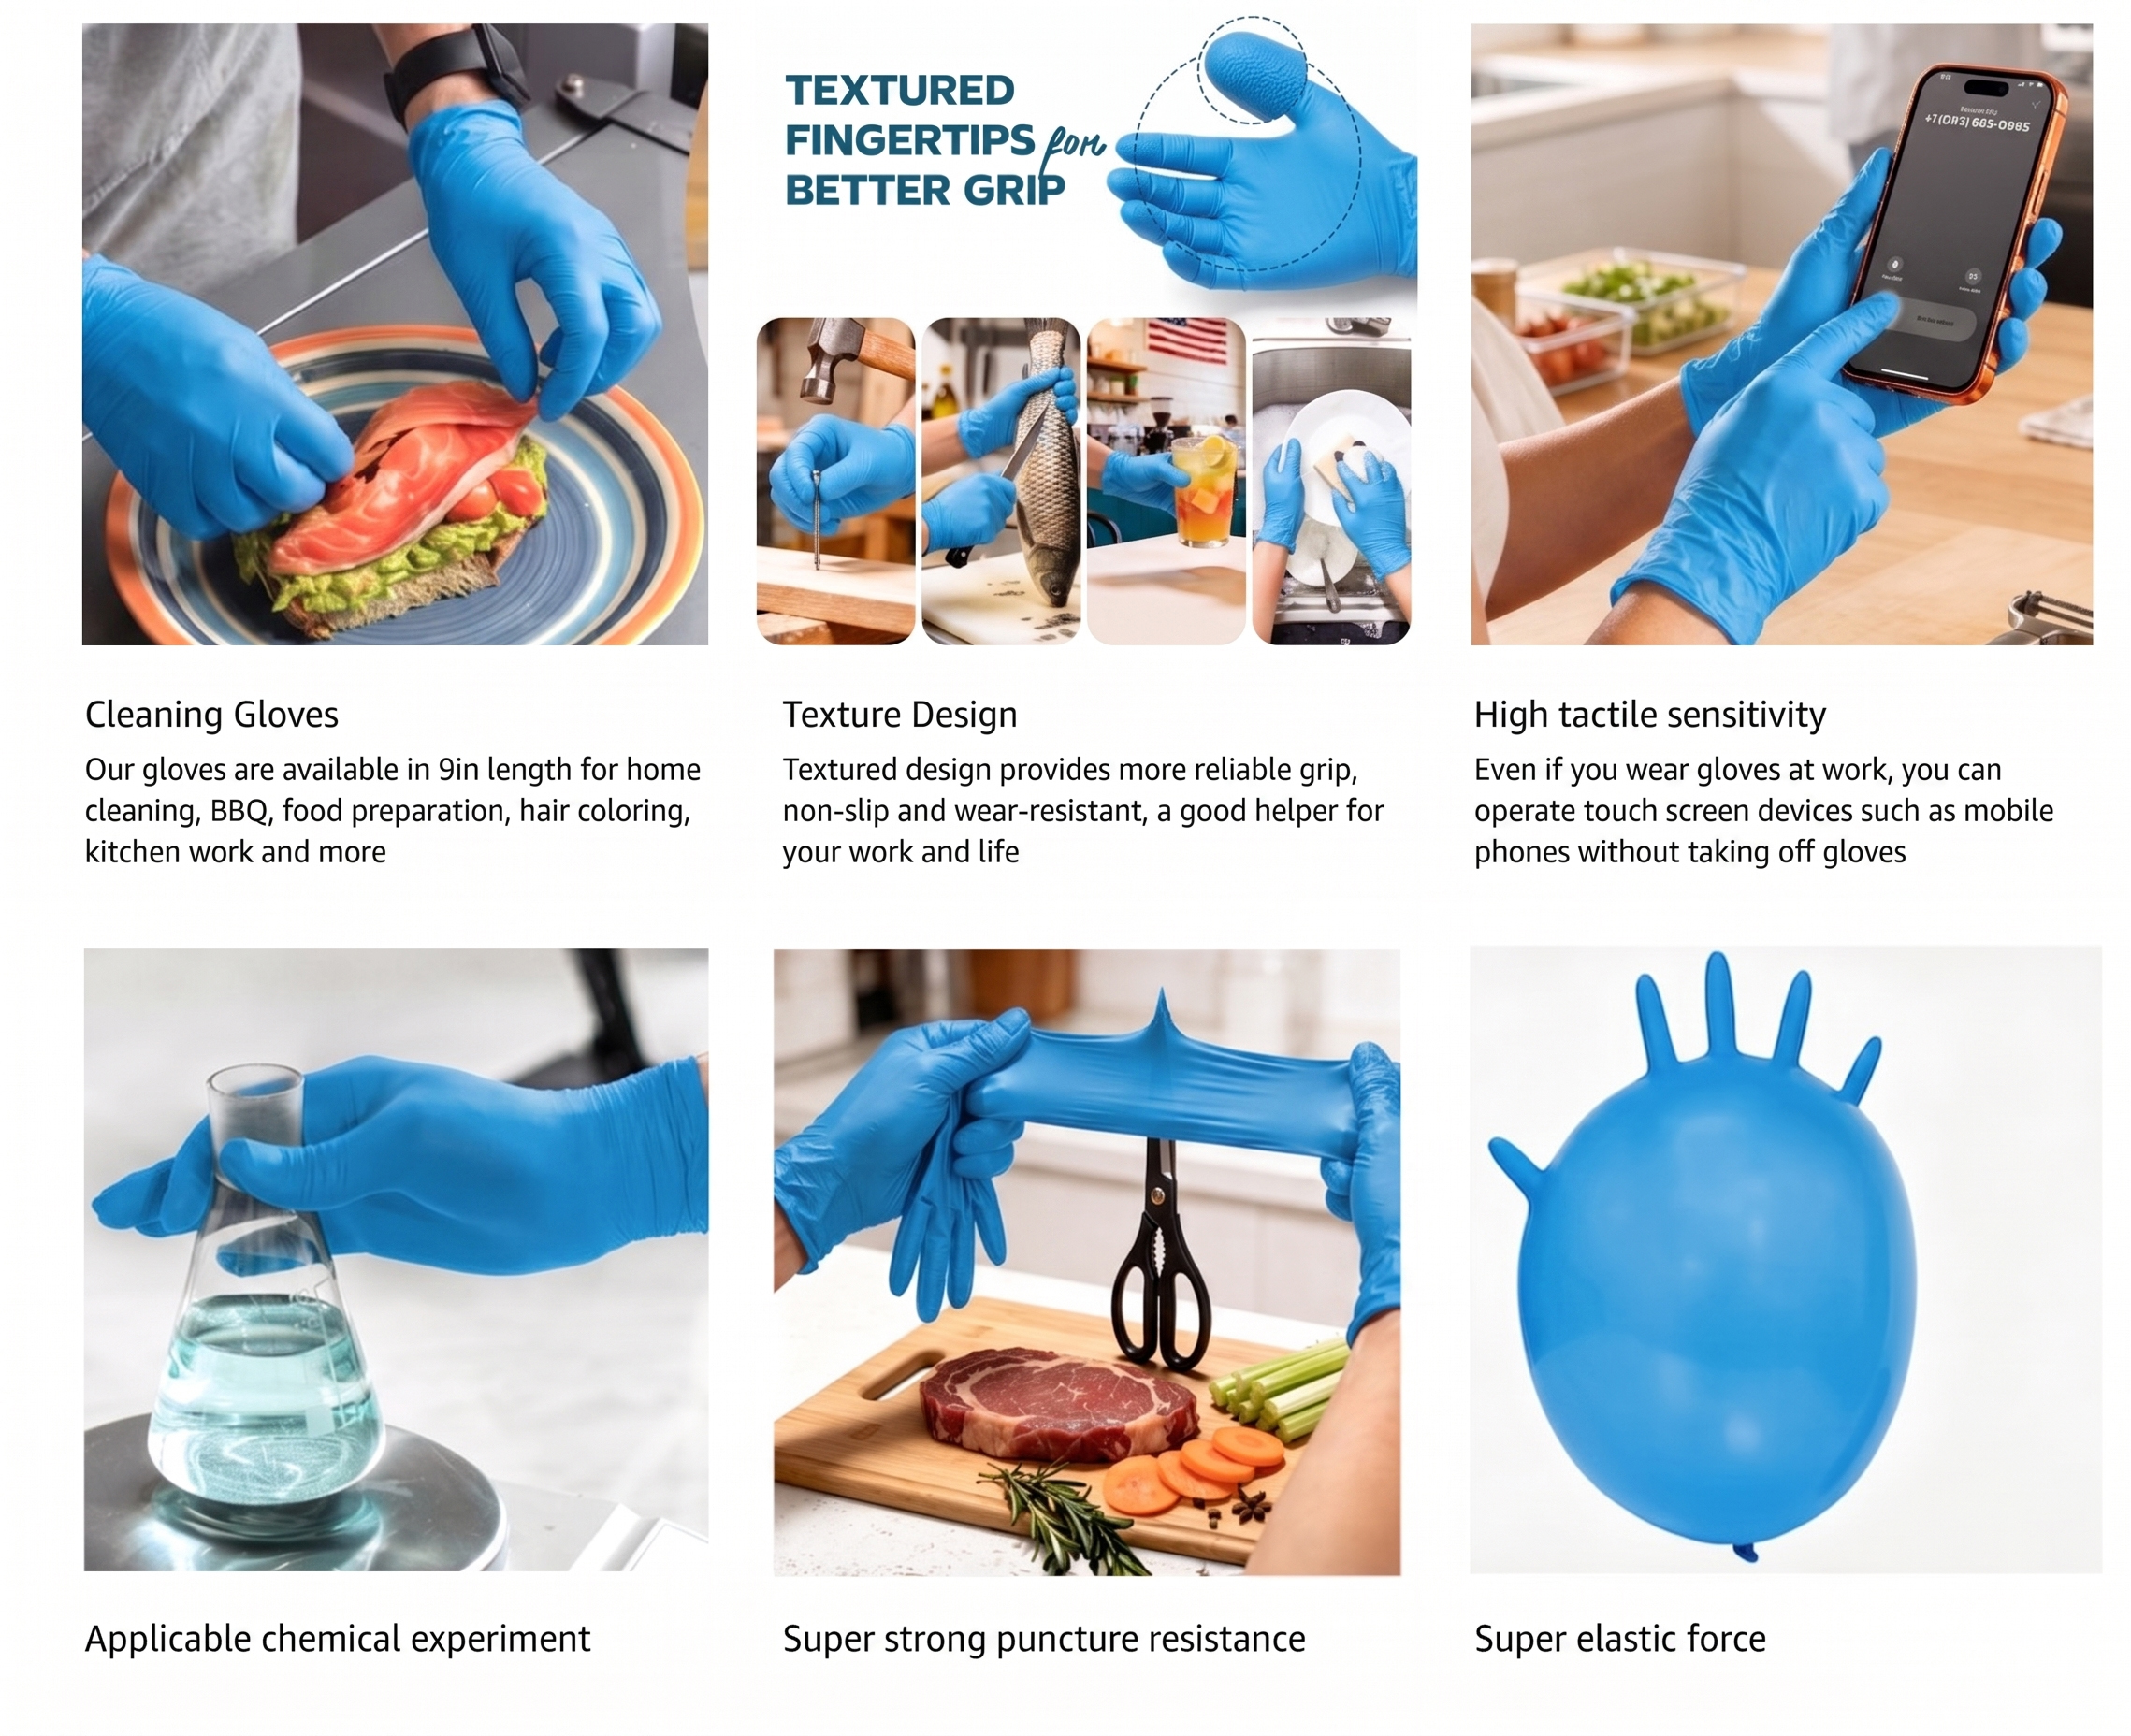
Can you operate a touch screen phone after wearing it
Yes, you can actually. I can show you nowIs this 100 pair or 100 gloves100 pieces glovesHow thick are they in mils10mil equal 0.26mm
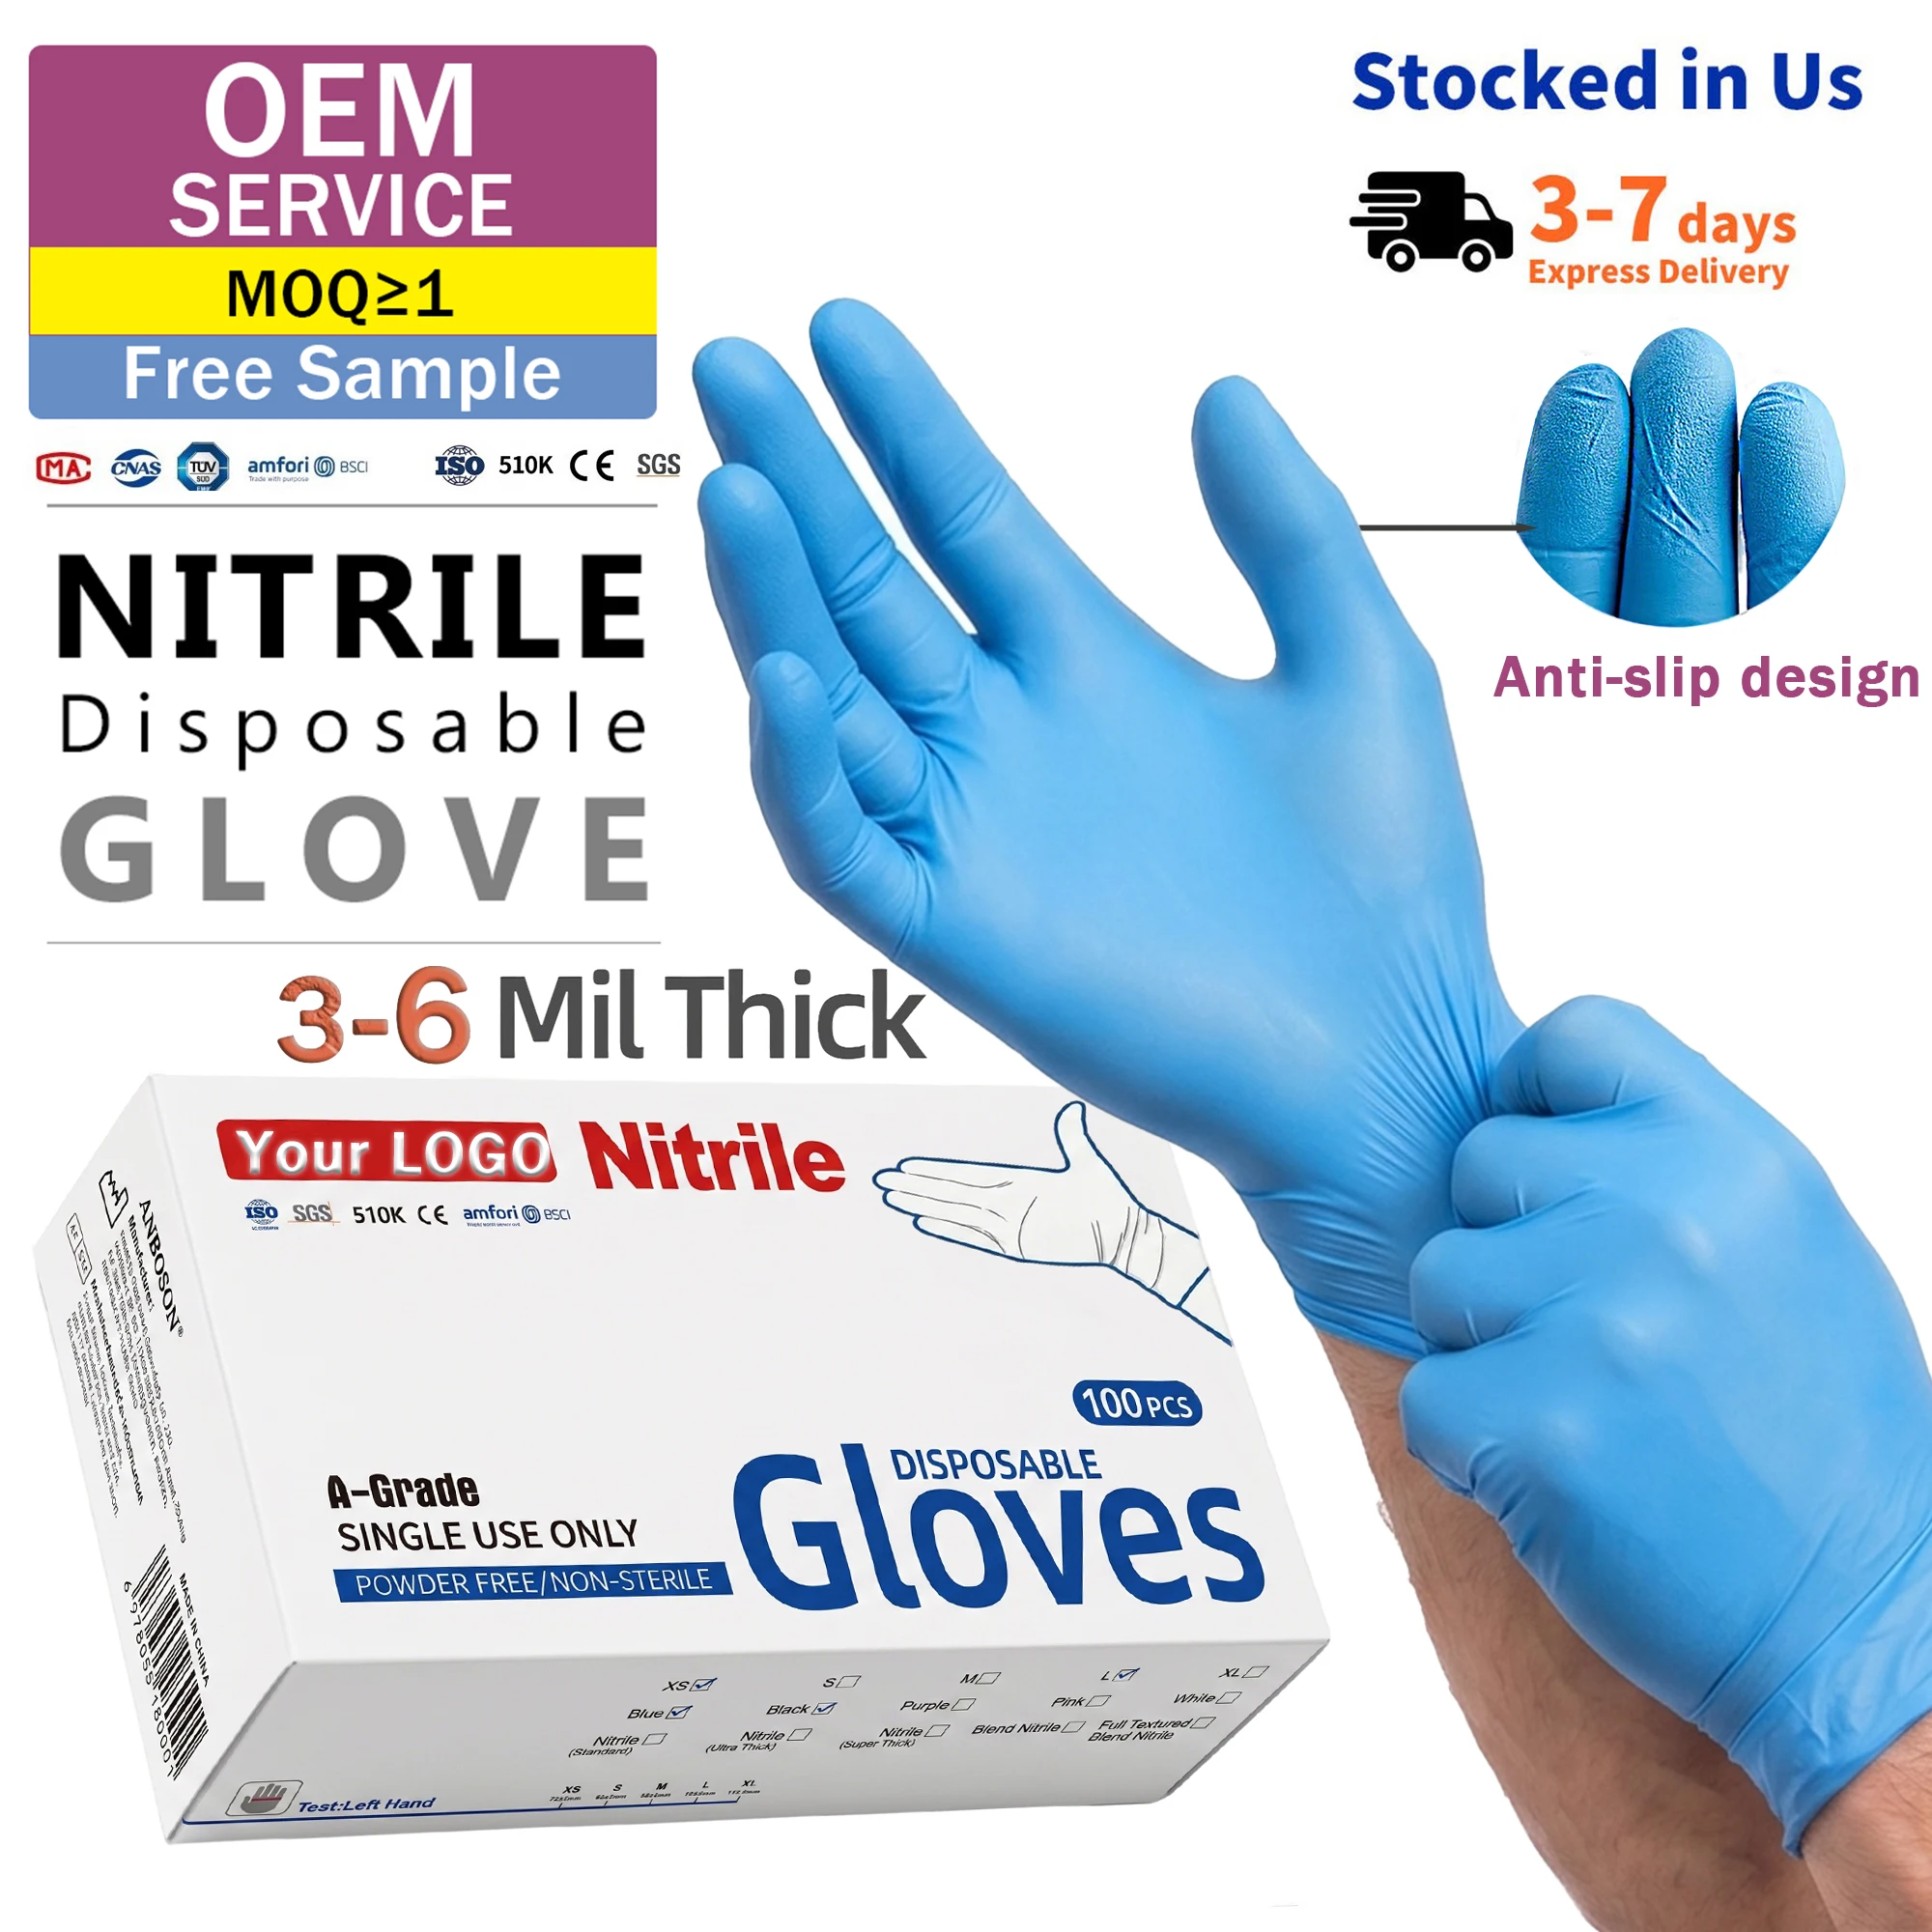
ANBOSON presents the 510K Custom Box 6mil Blue Nitrile Gloves Food Grade 100 Pcs Meat Processing Commercial Kitchens Guantes Para Cocina Wholesale, a purpose-built solution for food service professionals, commercial kitchen operators, and meat processing facilities seeking reliable protection and performance. Designed and manufactured by ANBOSON, a nitrile gloves specialist with 20 years of experience, this product blends food safety compliance, industrial-grade durability, and the tactile responsiveness professionals demand. This description outlines the product’s features, applications, innovations, and technical advantages while emphasizing why these 510K gloves are an essential element of modern commercial kitchen PPE.
Product Overview and Target Use
ANBOSON’s 510K gloves are 6mil blue nitrile, packaged in a custom box of 100 pieces to meet the throughput and safety needs of busy food preparation environments. These food grade nitrile gloves are intended for repetitive handling tasks in meat processing, deli counters, bakery lines, and full-service commercial kitchens. The blue color provides high visibility to help prevent cross-contamination and accidental glove fragments in food, meeting the expectations of food service managers and inspectors. As essential commercial kitchen PPE, these gloves support hygiene protocols and food safety programs in restaurants, catering services, institutional kitchens, and wholesale meat processors.
Key Features
- Food grade nitrile construction: Manufactured with materials formulated to comply with stringent food safety standards, these 510K gloves are suitable for direct contact with food items. The formulation avoids latex proteins, reducing the risk of allergic reactions among staff and consumers while preserving barrier integrity during handling.
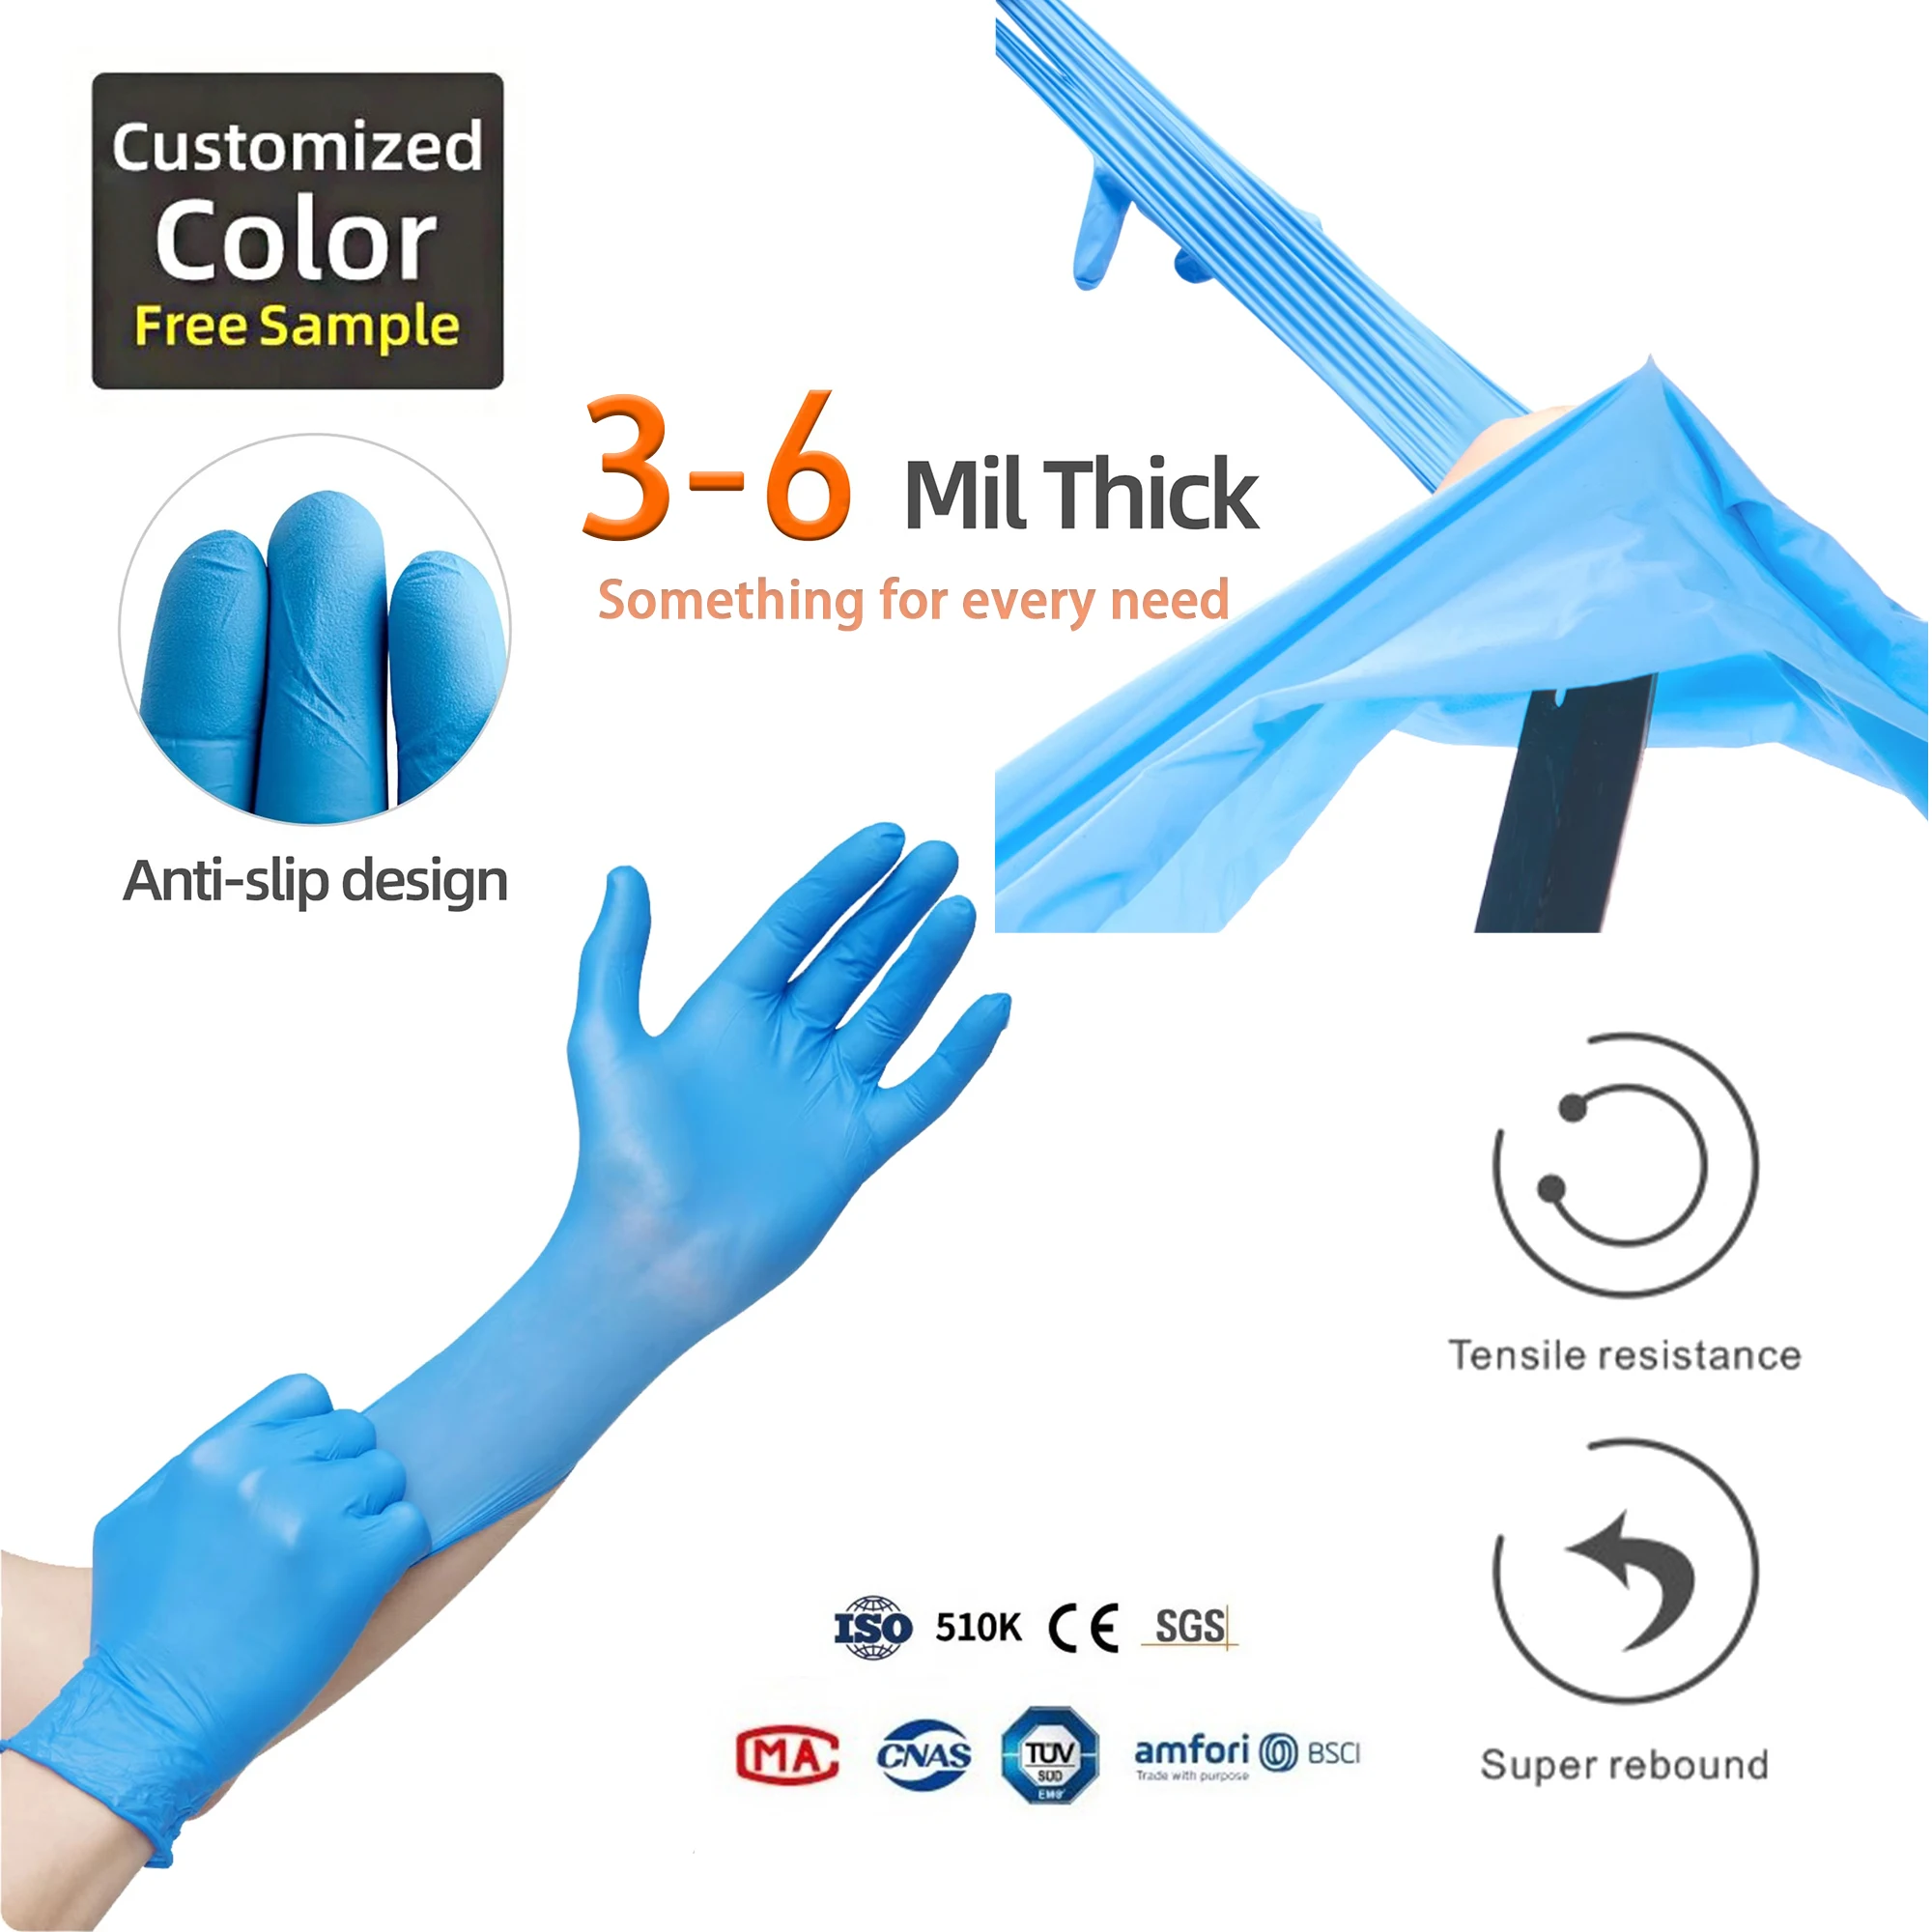
- 6mil thickness: The 6mil blue nitrile specification provides a balanced combination of tactile sensitivity and puncture resistance. This thickness makes the gloves suitable for precision tasks such as portioning, trimming, and plating while offering robust protection against oils, fats, and abrasion common in meat processing and commercial kitchens.
- 510K clearance and compliance-oriented design: The 510K designation signals regulatory compliance for food contact and professional use where such clearances are requested. Combining regulatory awareness with practical design, these gloves support food safety programs and facility audits.
- Powder-free and chlorinated finish: The gloves are processed with advanced chlorination technology, yielding a powder-free surface that eases donning and reduces contamination risks. This finish also improves grip under wet and oily conditions, a critical advantage in kitchen environments.
- High-visibility blue color: Blue is an industry-recognized color for food handling gloves due to its ease of detection. The blue nitrile color helps kitchen staff quickly identify glove use and enables automated or manual foreign object detection systems to spot glove fragments more easily.
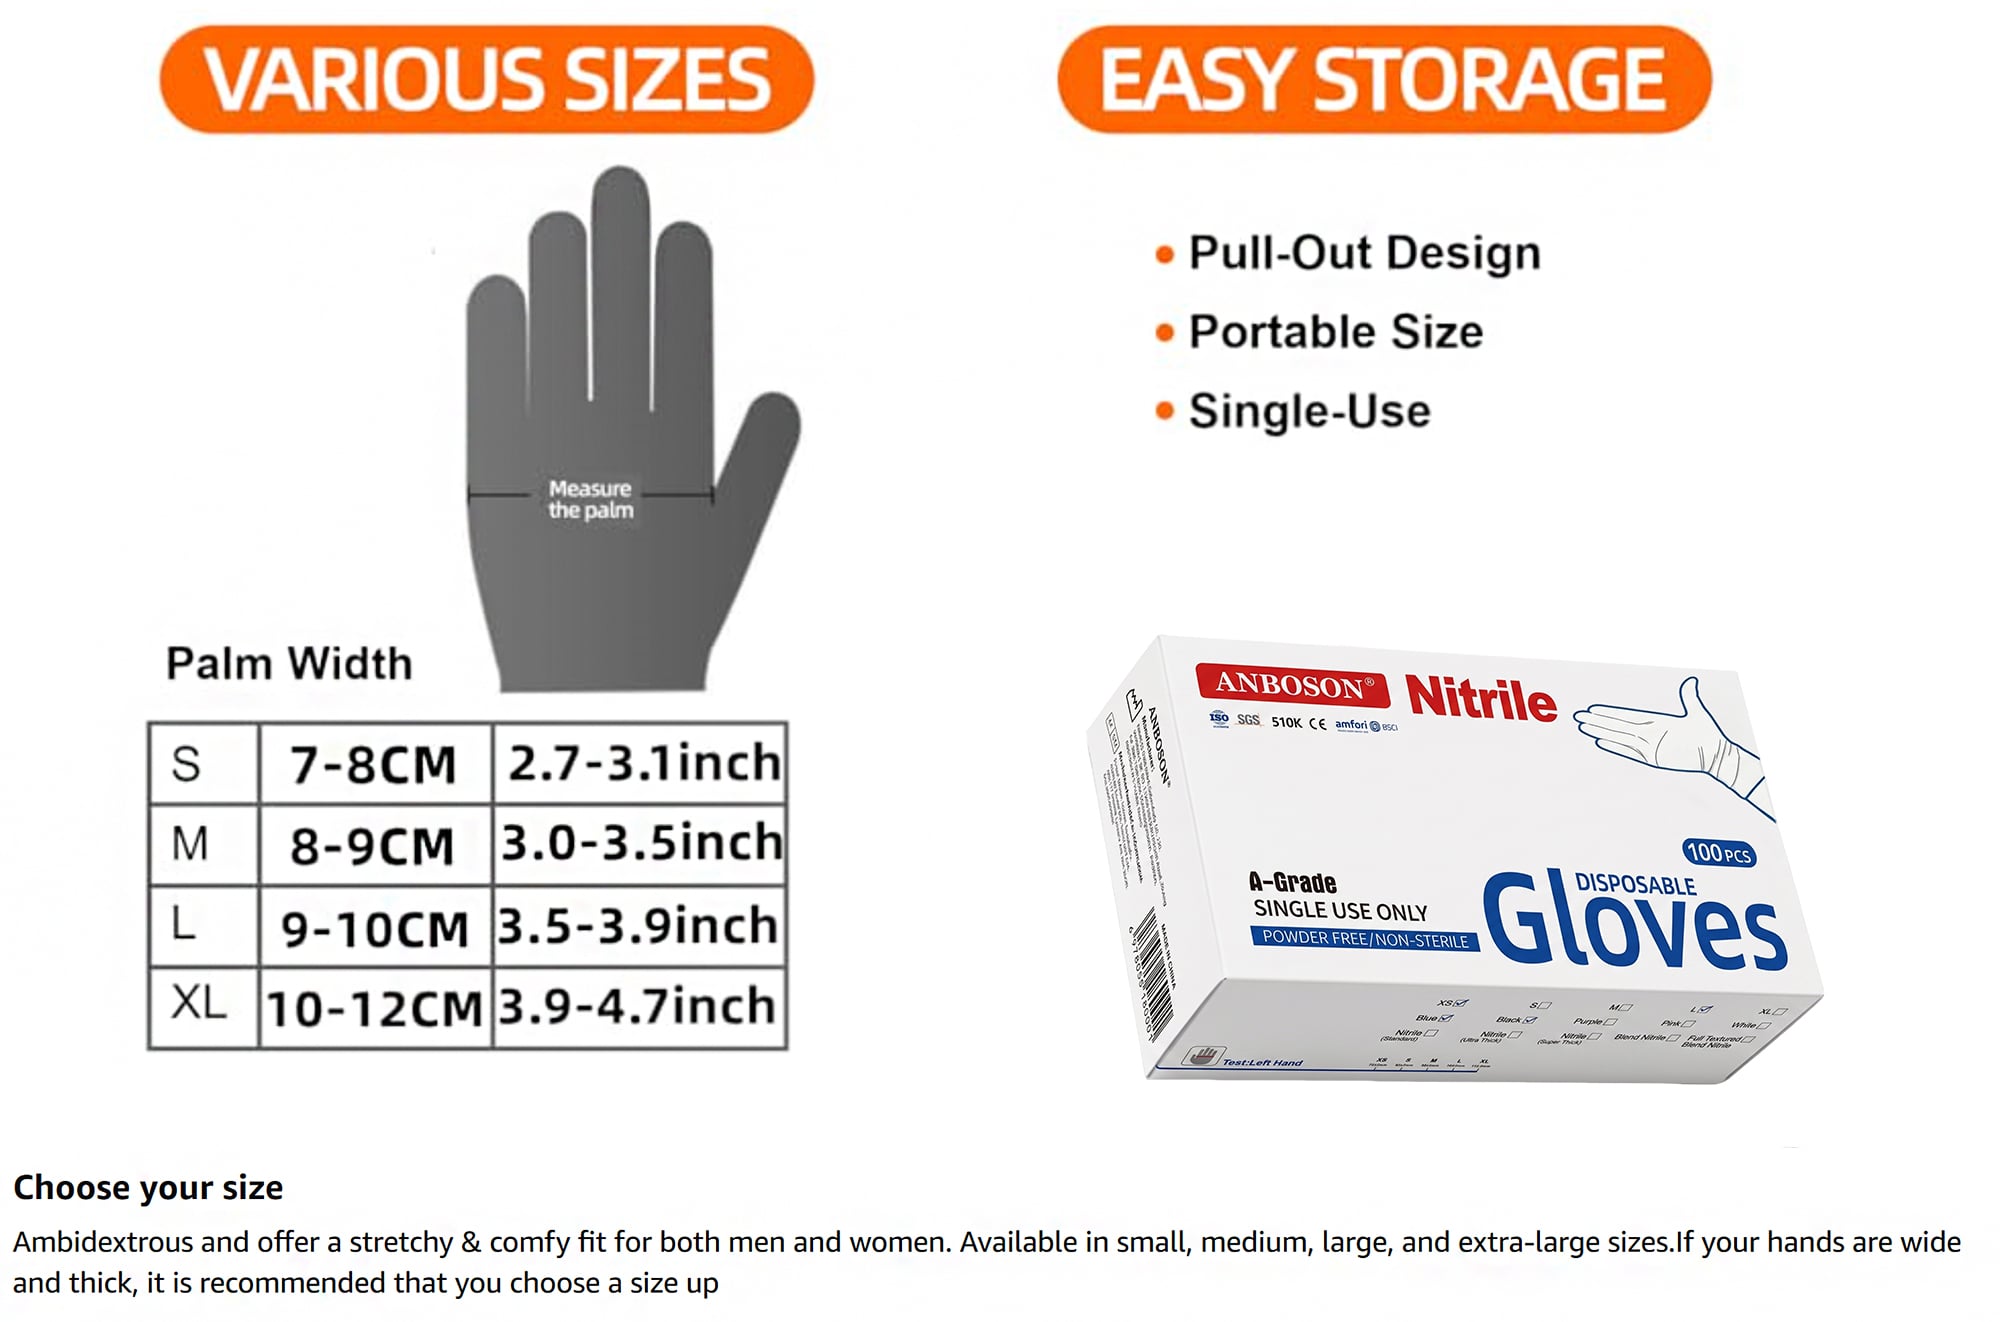
- Custom box packaging: Each box of 100 pcs is designed for convenience in high-volume environments.
Applications and Use Cases
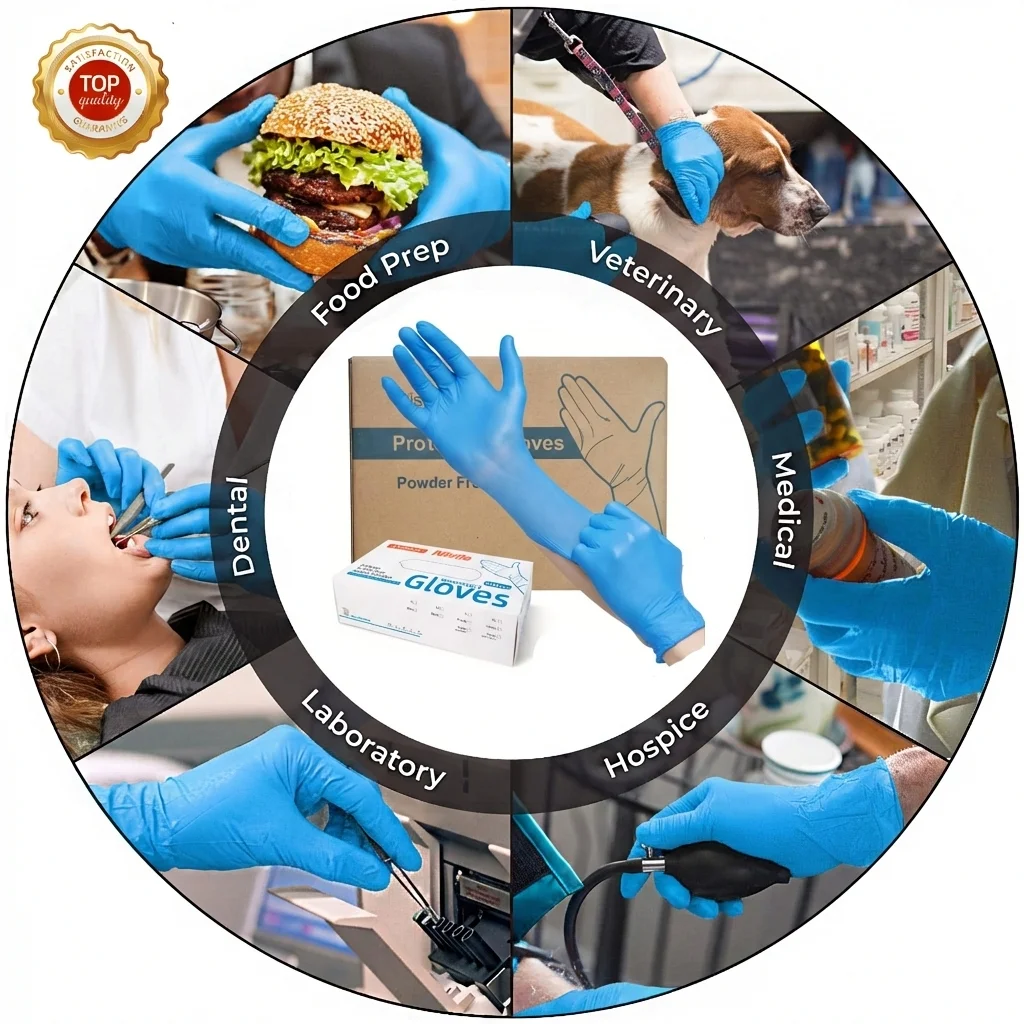
These 510K gloves are optimized for diverse applications across food production and service:
- Meat processing: Ideal for trimming, portioning, and packaging meat products where resistance to oils and animal fats is crucial. The 6mil blue nitrile delivers durability and puncture resistance required for repetitive cutting and handling.
- Commercial kitchen operations: From line cooks to prep stations, the gloves serve as primary commercial kitchen PPE for safe, hygienic food handling in restaurants, hotels, and institutional cafeterias.
- Food retail and deli counters: For servers and butchers working at counters, these gloves combine dexterity and food grade features that maintain both safety and customer service speed.
- Catering and food service events: Disposable, reliable gloves reduce cross-contamination risk during temporary or high-volume service events, where rapid glove changes and consistent hygiene are essential.
- Wholesale and cold-chain environments: Packaging and loading tasks in wholesale food distribution benefit from the gloves’ oil resistance and low-temperature performance, supporting safer handling throughout the supply chain.
Performance and Technical Advantages
ANBOSON leverages two decades of nitrile expertise and industrial-scale manufacturing capabilities to deliver performance advantages that matter to food service operators:
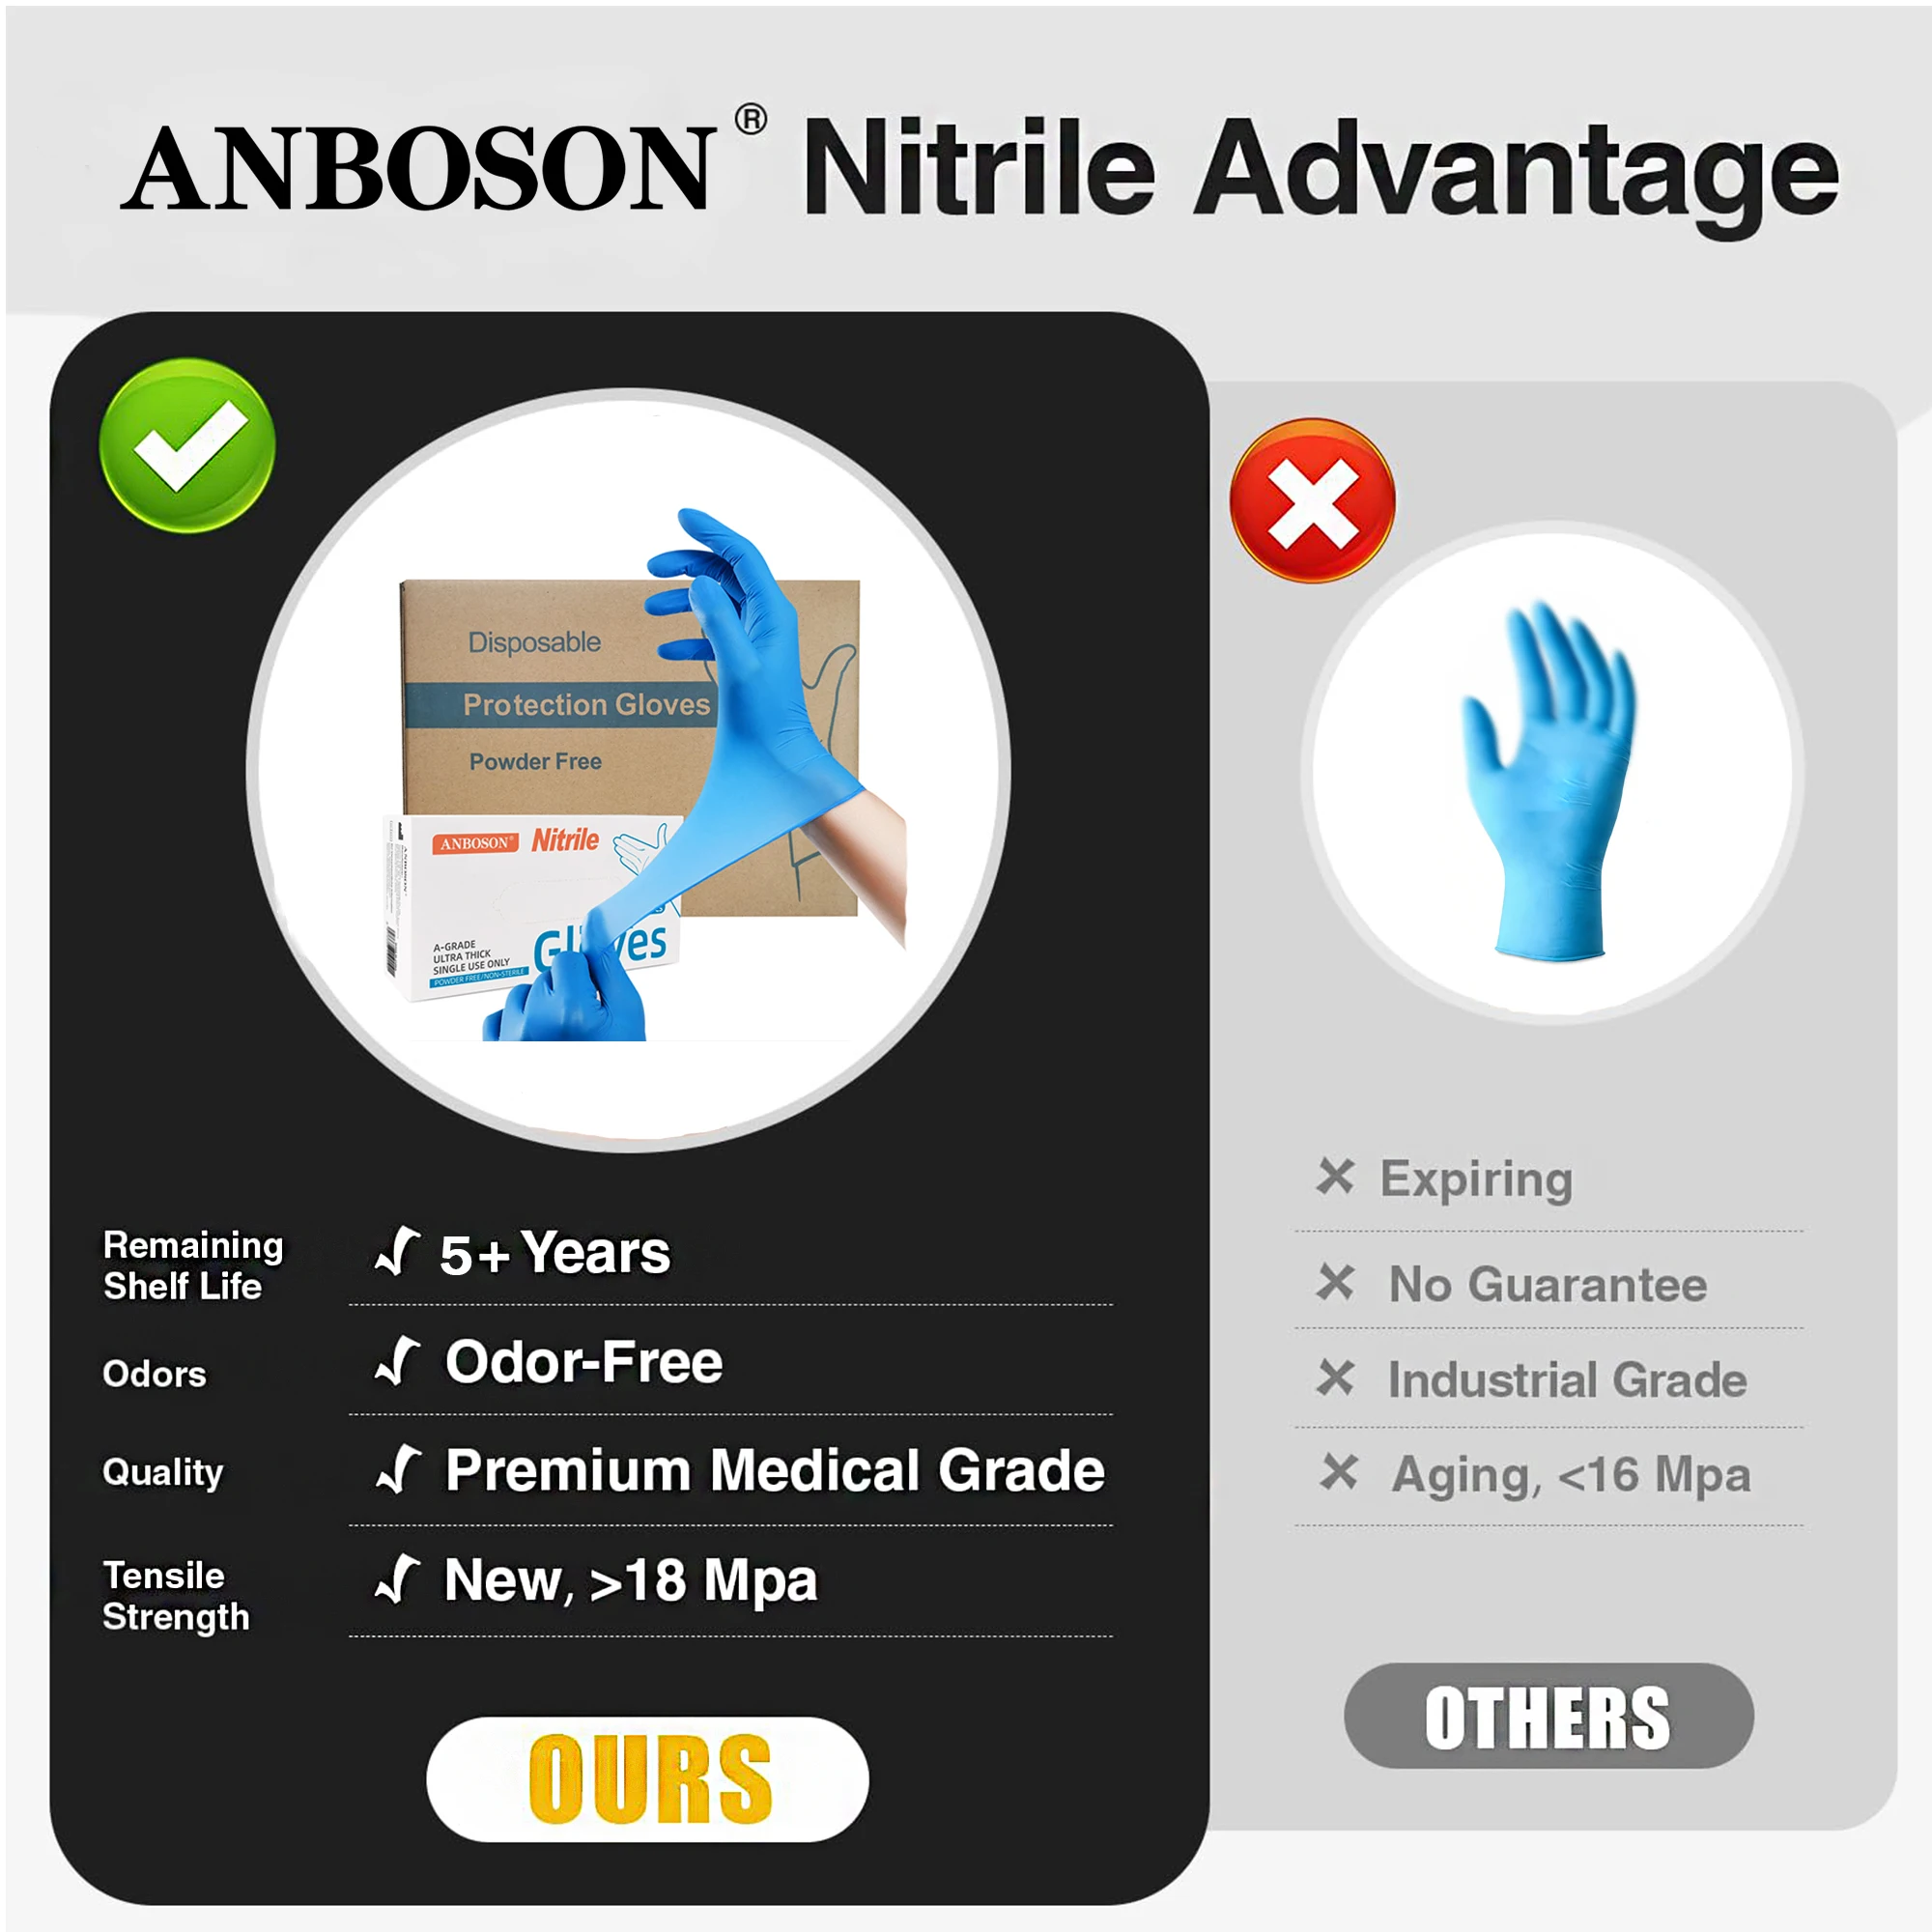
- Enhanced tensile and puncture resistance: Formulated to resist tears and punctures common in meat processing environments, the 6mil blue nitrile composition supports sustained use during intense workflows, reducing replacement frequency and waste.
- Oil and aging resistance: Proprietary material blends and processing create a glove with improved resistance to oils, solvents commonly found in food processing, and long-term aging, ensuring consistent performance over the glove’s shelf life.
- Chlorination for improved donning and grip: ANBOSON’s advanced chlorination process removes surface tack and enhances donning ease while improving grip performance in wet and oily conditions—critical properties for safe, efficient food handling.
- ISO and CE-aligned quality systems: Manufactured in facilities adhering to ISO and CE frameworks, ANBOSON’s production processes and quality control systems ensure consistent glove thickness, strength, and food-contact safety.
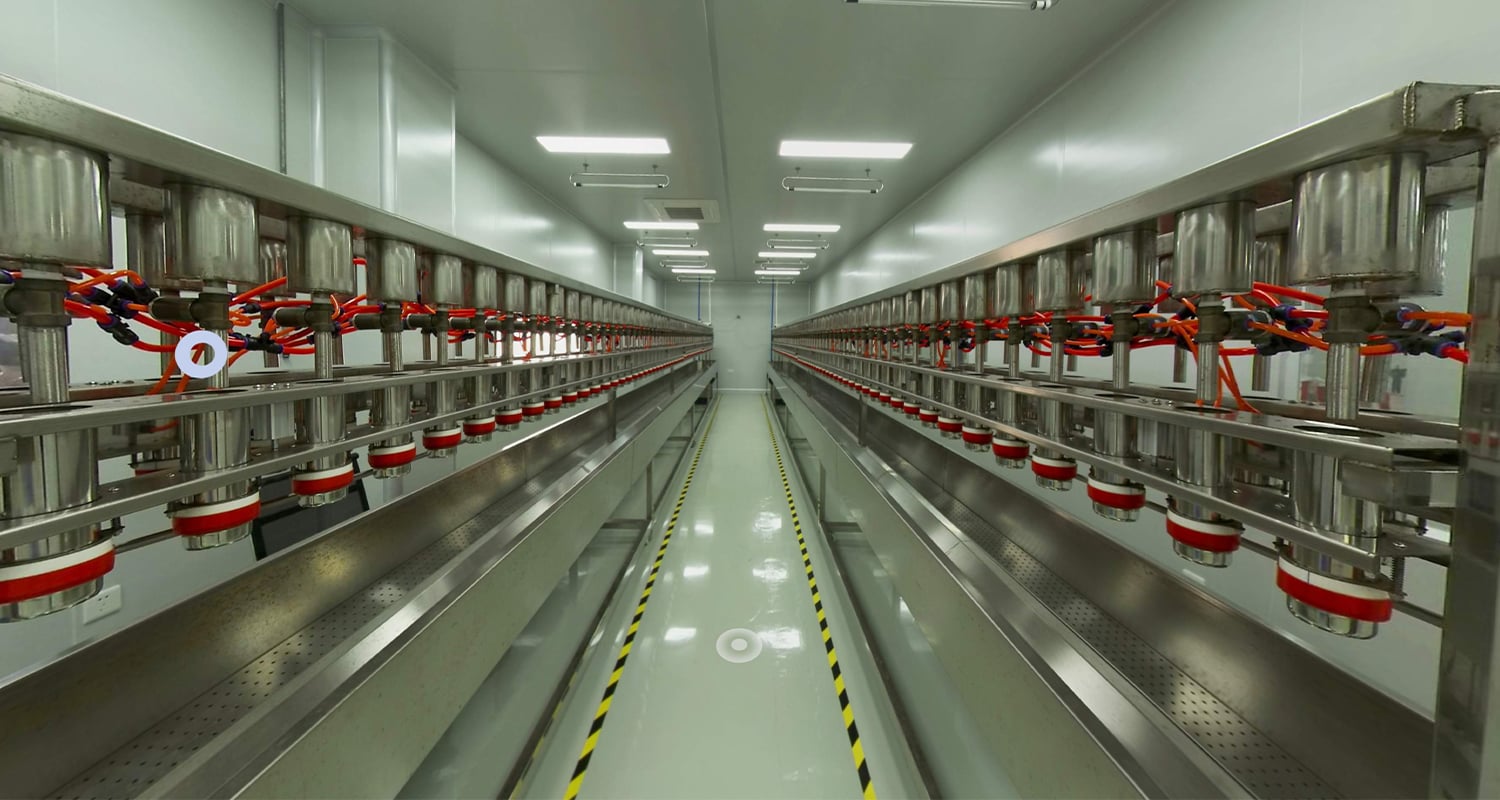
- Robust production capacity and reliable supply: With six production lines and an annual output of 4.8 billion gloves, ANBOSON can reliably supply large operations and support OEM/ODM customization for businesses requiring branded or specialized packaging solutions.
Innovation Highlights
ANBOSON’s innovations in manufacturing and material science translate to practical benefits for food handlers:
- Optimized nitrile formulations: Continuous refinement of nitrile compounds results in gloves that balance thinness for tactile tasks with strength for durability. The 6mil blue nitrile design exemplifies this balance.
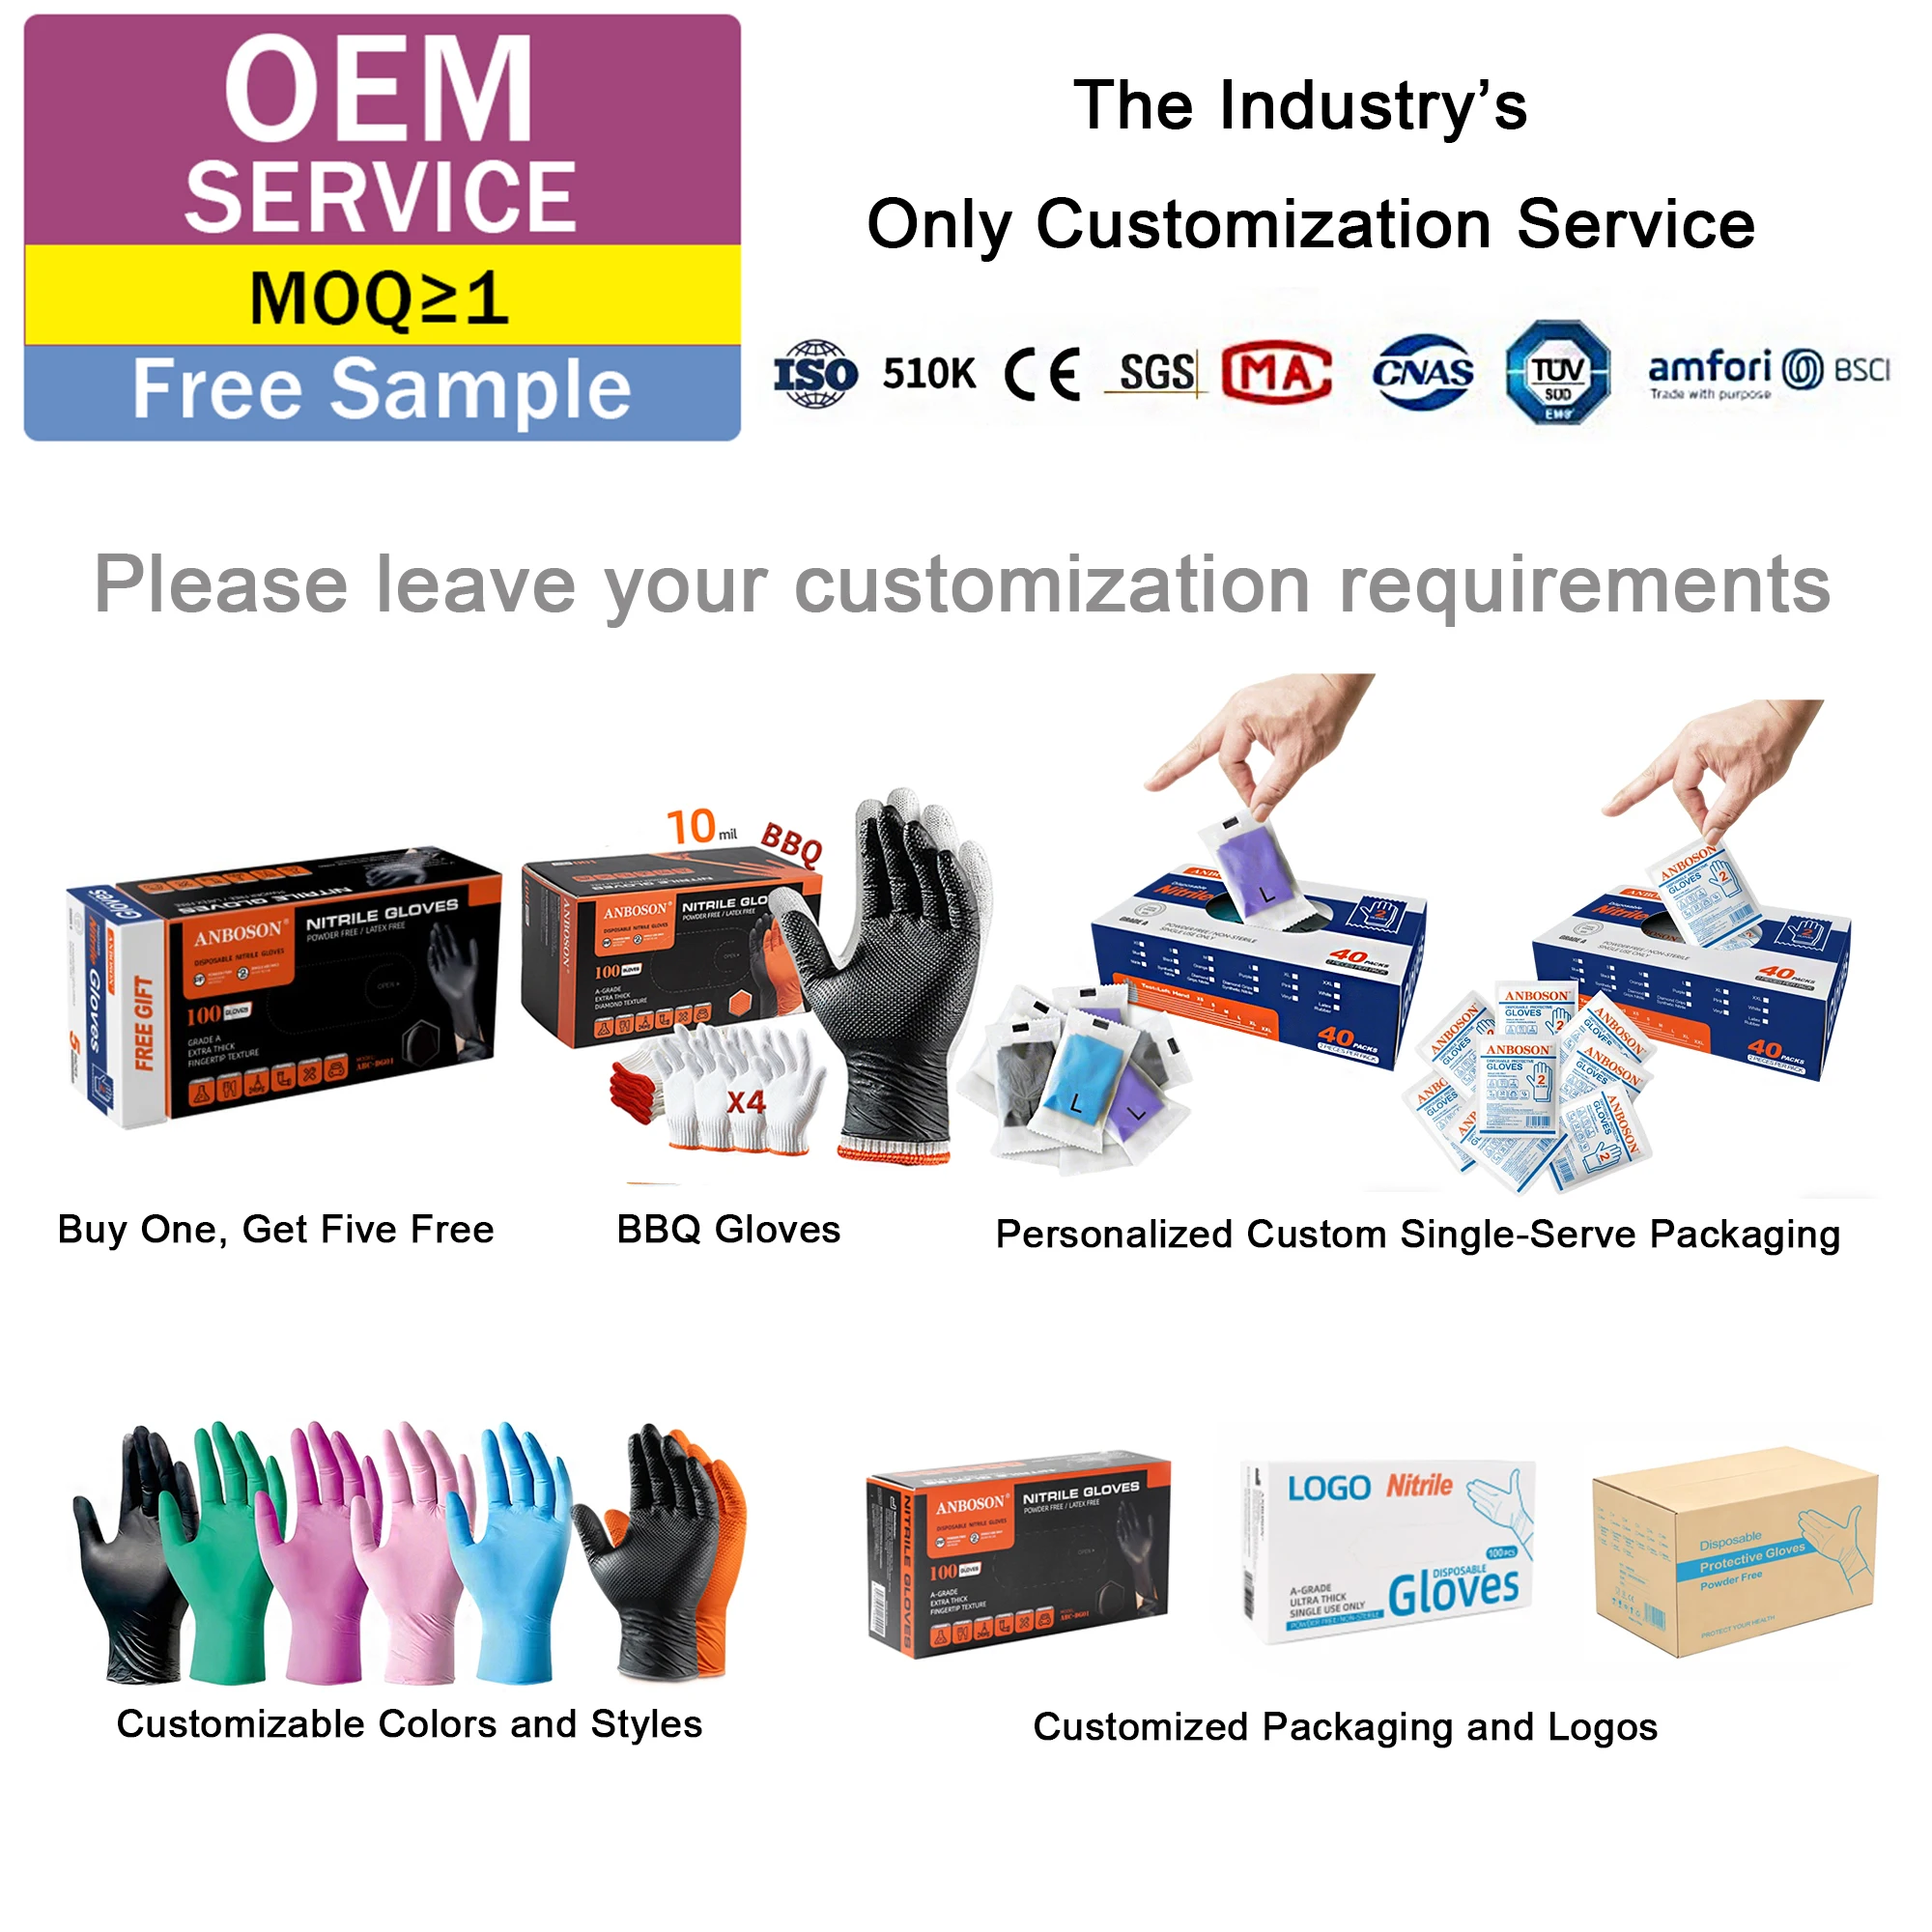
- Scalable customization: ANBOSON supports box and product customization to fit client needs, from private-label solutions to specialized packaging for different foodservice scenarios.
- Process consistency via advanced chlorination: The chlorination method employed by ANBOSON enhances both user comfort and in-use performance, delivering a product that meets the demanding conditions of commercial kitchens without compromising safety.
Why Choose ANBOSON 510K Gloves
- Food safety first: These 510K gloves are specifically formulated for food contact, offering confidence in environments where hygiene and contamination control are paramount.
- Purpose-built for commercial kitchen PPE: The gloves are engineered to meet the practical needs of chefs, line cooks, butchers, and food handlers requiring both dexterity and protection.
- Proven manufacturing pedigree: Backed by two decades of expertise and high-volume, quality-oriented production, ANBOSON delivers consistent product quality and supply reliability to food industry partners.
- Cost-effective durability: The 6mil thickness reduces tear-through and waste, delivering a reliable single-use option that supports operational efficiency and staff safety
For facilities that prioritize food safety, operational efficiency, and dependable protective equipment, the ANBOSON 510K Custom Box 6mil Blue Nitrile Gloves Food Grade 100 Pcs Meat Processing Commercial Kitchens Guantes Para Cocina Wholesale represent a practical and compliant choice. Combining food grade nitrile construction, visible blue coloring, powder-free chlorinated finish, and manufacturing excellence, these gloves meet the stringent demands of modern foodservice operations and commercial kitchen PPE programs.

FDA 510K · CE · ISO 13485 · SGS — fully certified to meet global medical and industrial standards.

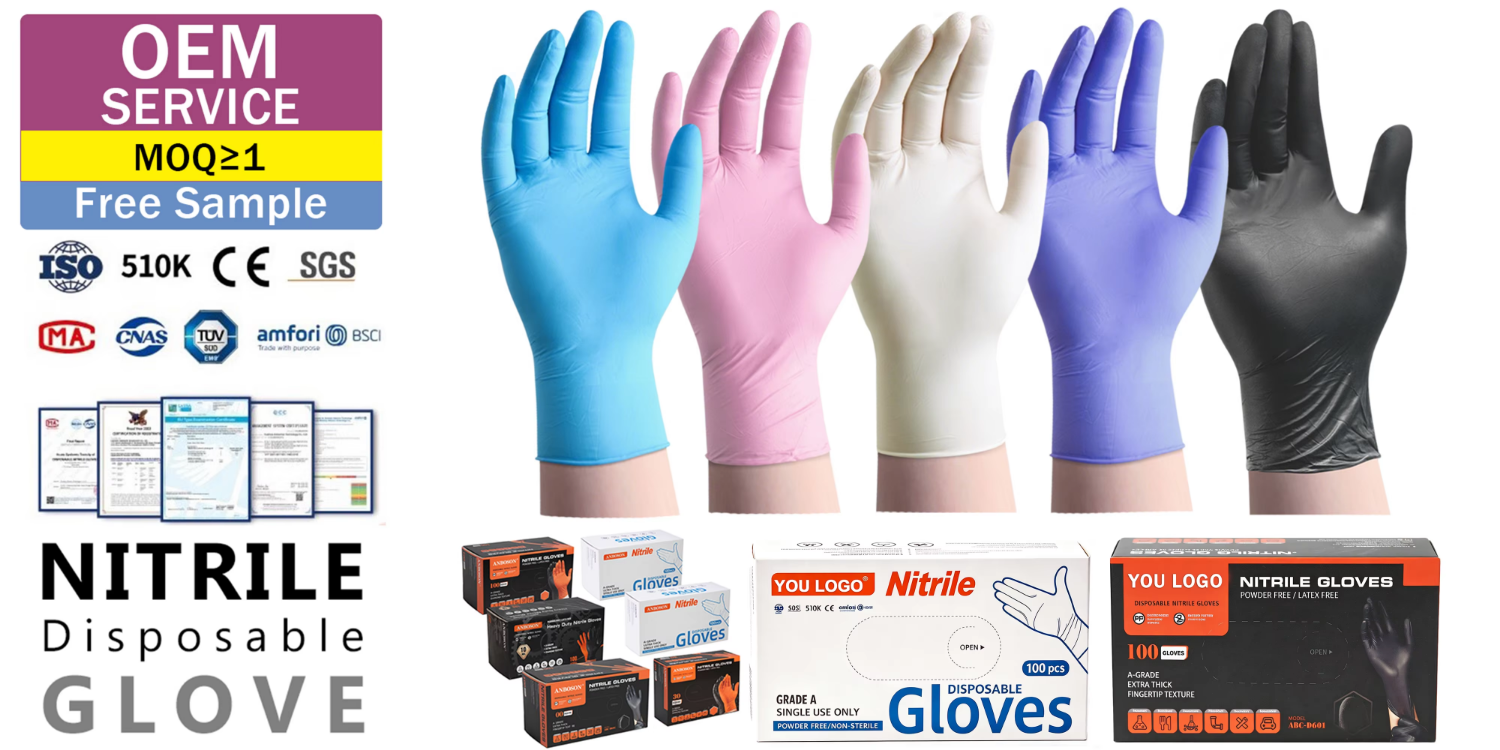
Automated factory with 100% quality inspection and double-dipping technology for extra strength and consistency.

Start small with low minimum order quantities and free samples — test our quality with zero risk.

Your logo, your colors, your specs — custom packaging, printing, thickness, and length to match your brand.
From hospital wards to food production lines, our medical gloves and disposable products deliver certified, dependable protection across every environment that demands it.

Certified protection for staff and patients in high-risk clinical settings

Chemical-safe handling engineered for demanding lab workflows

Strict hygiene standards, maintained from line to packaging

Reliable barrier protection for every procedure and every patient